INQUIRE NOW
On site PSA nitrogen generation from 95 to 99.9995 percent purity, engineered to your process rather than a fixed catalog spec.
Inquiry
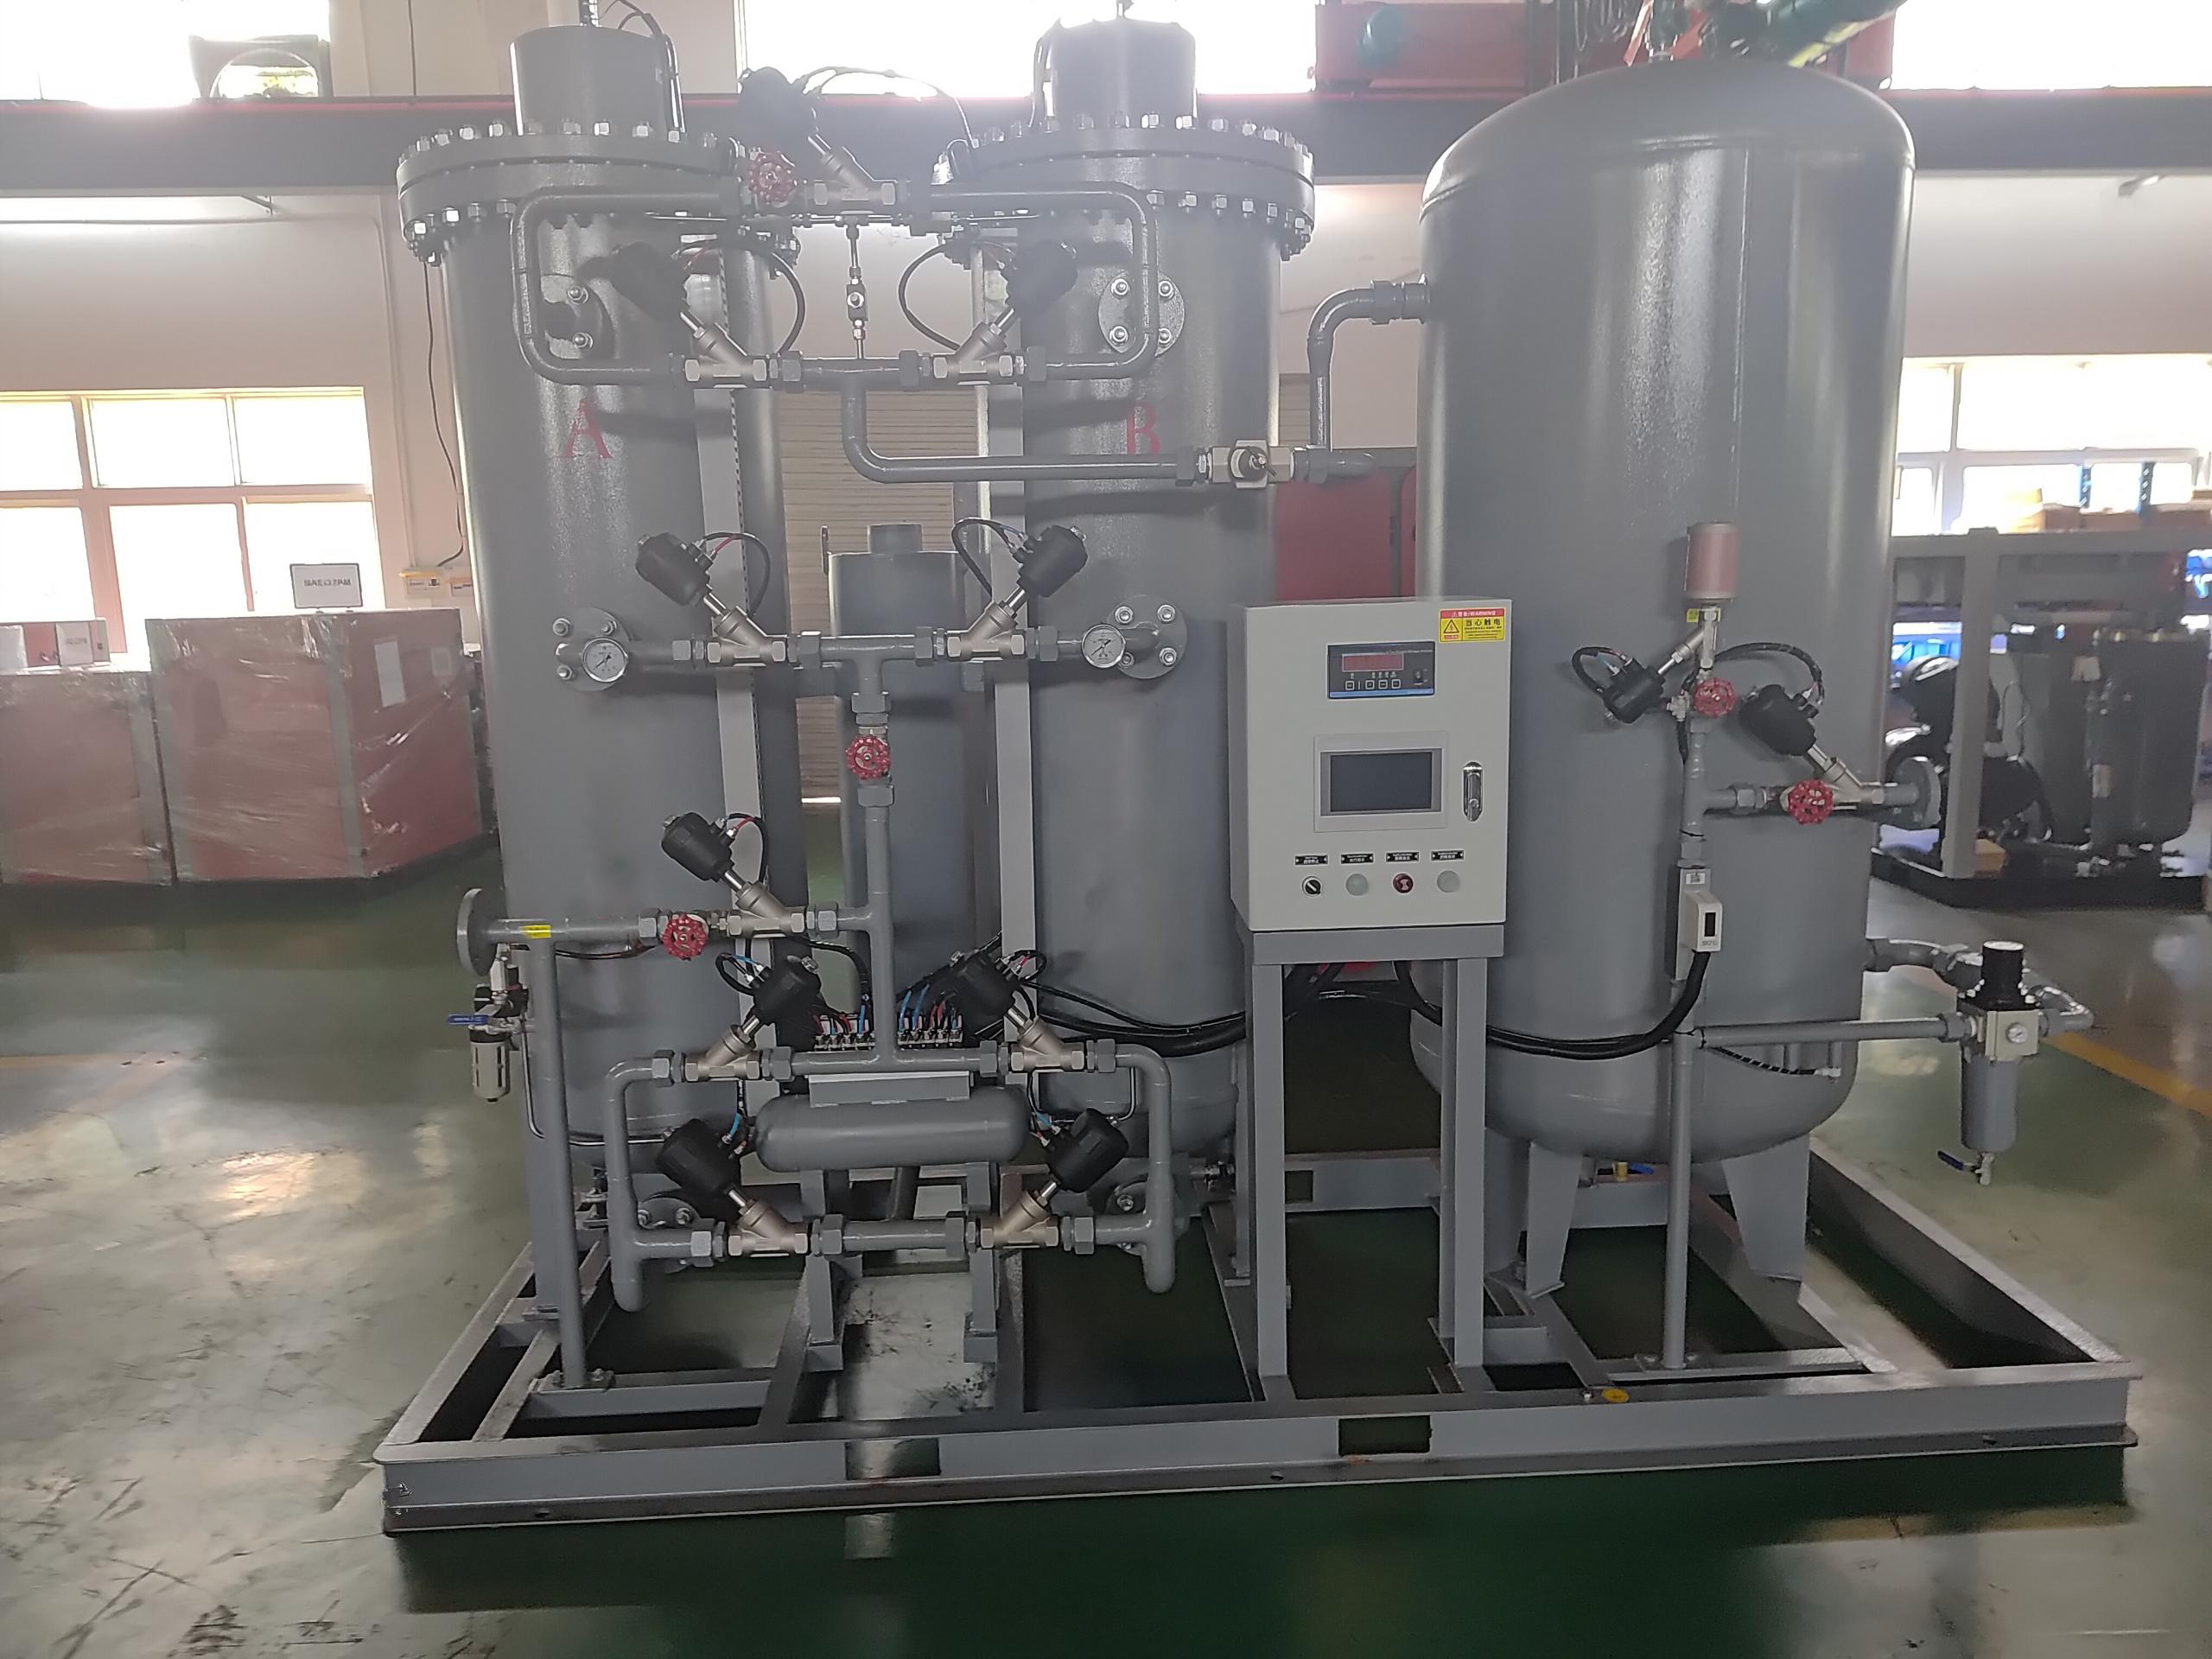
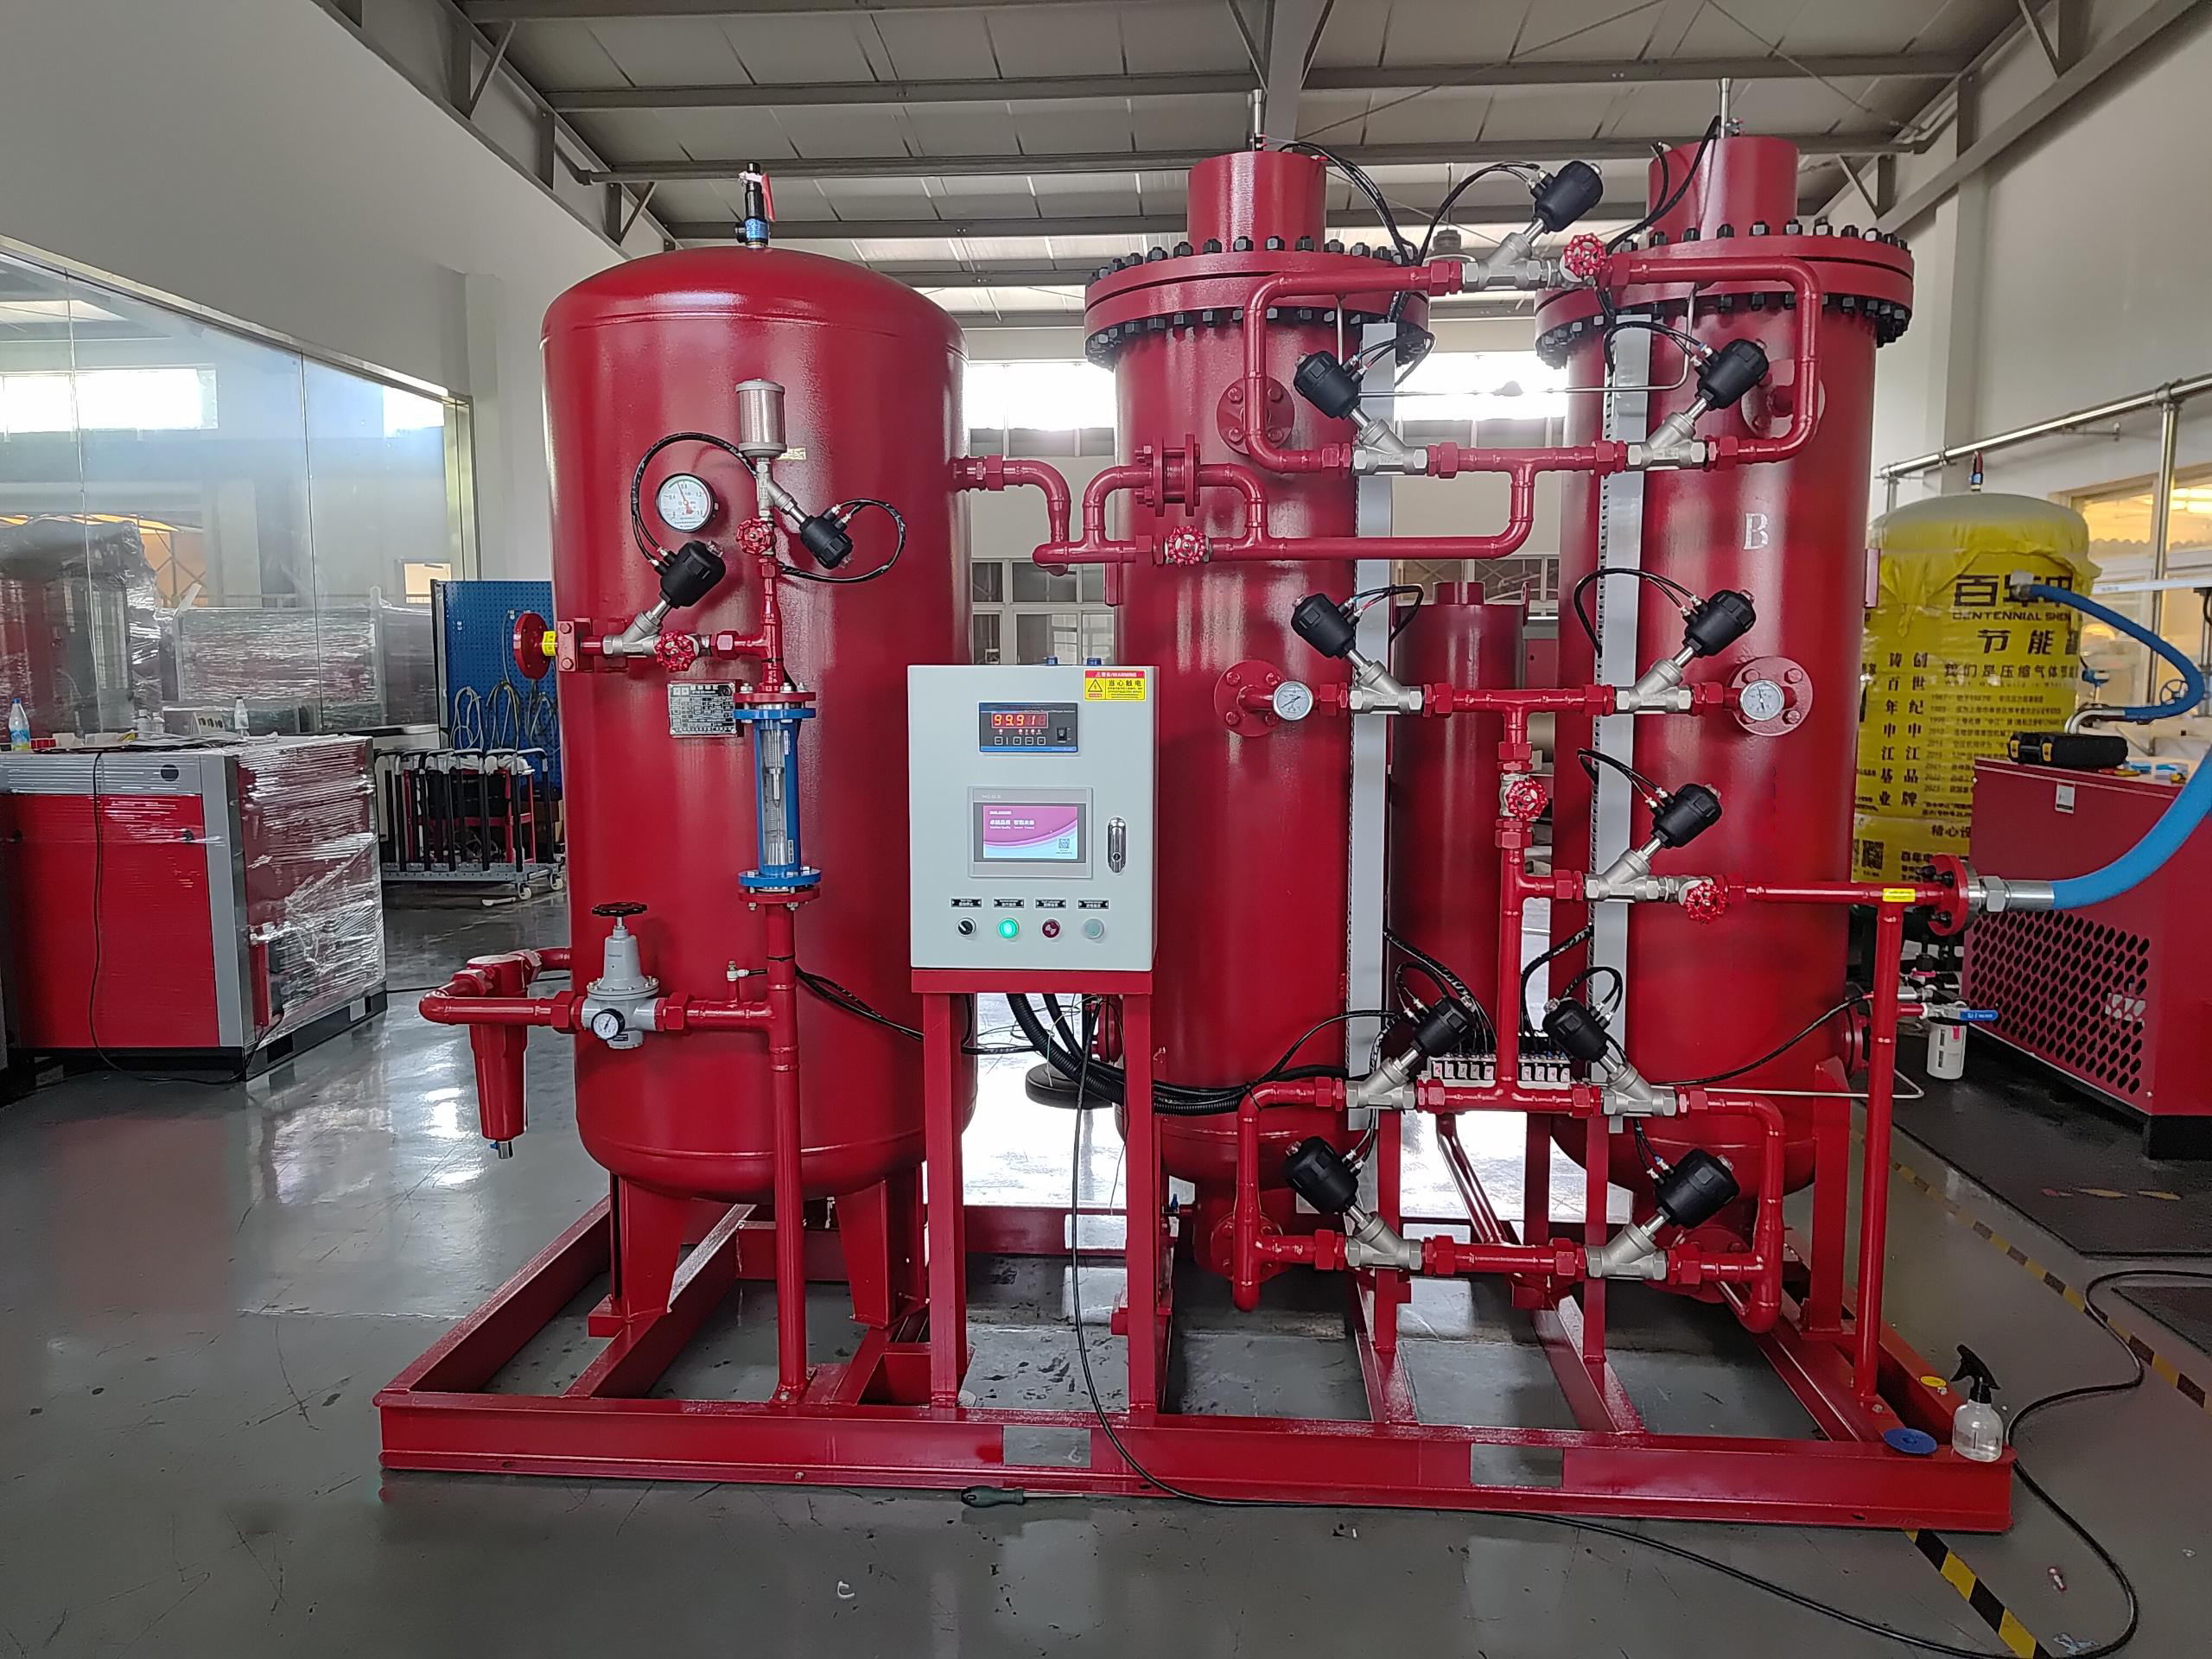
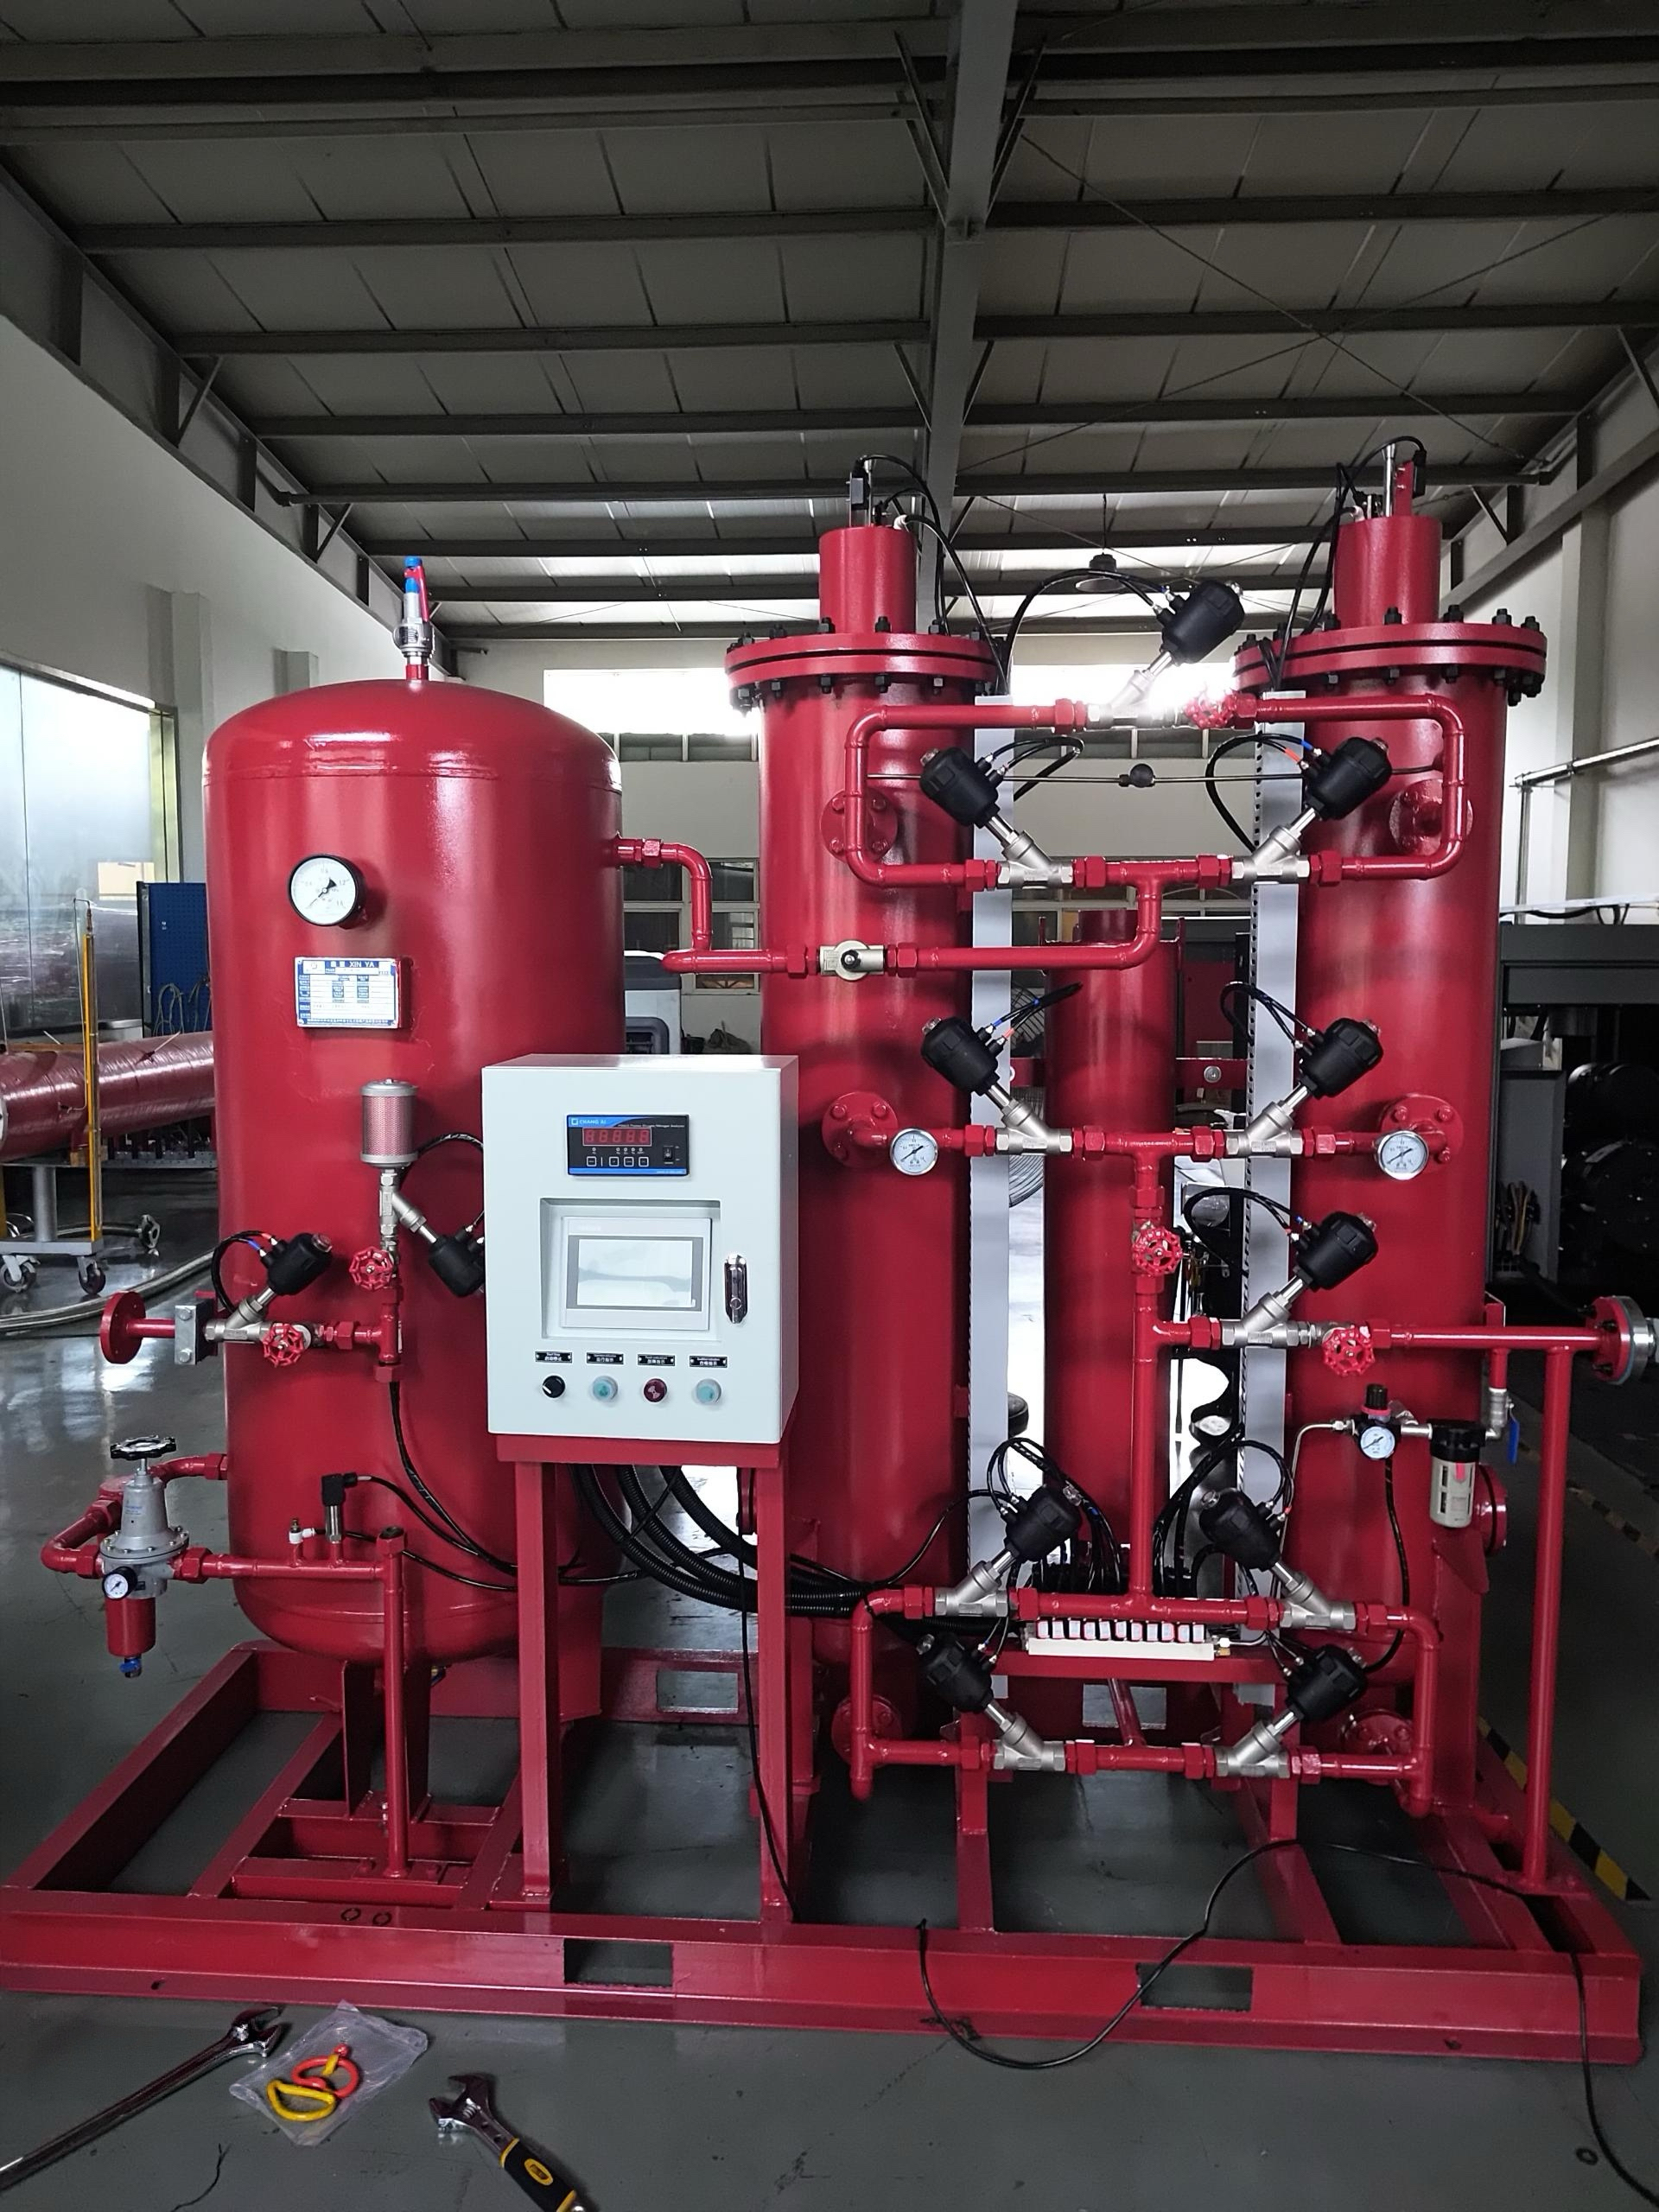
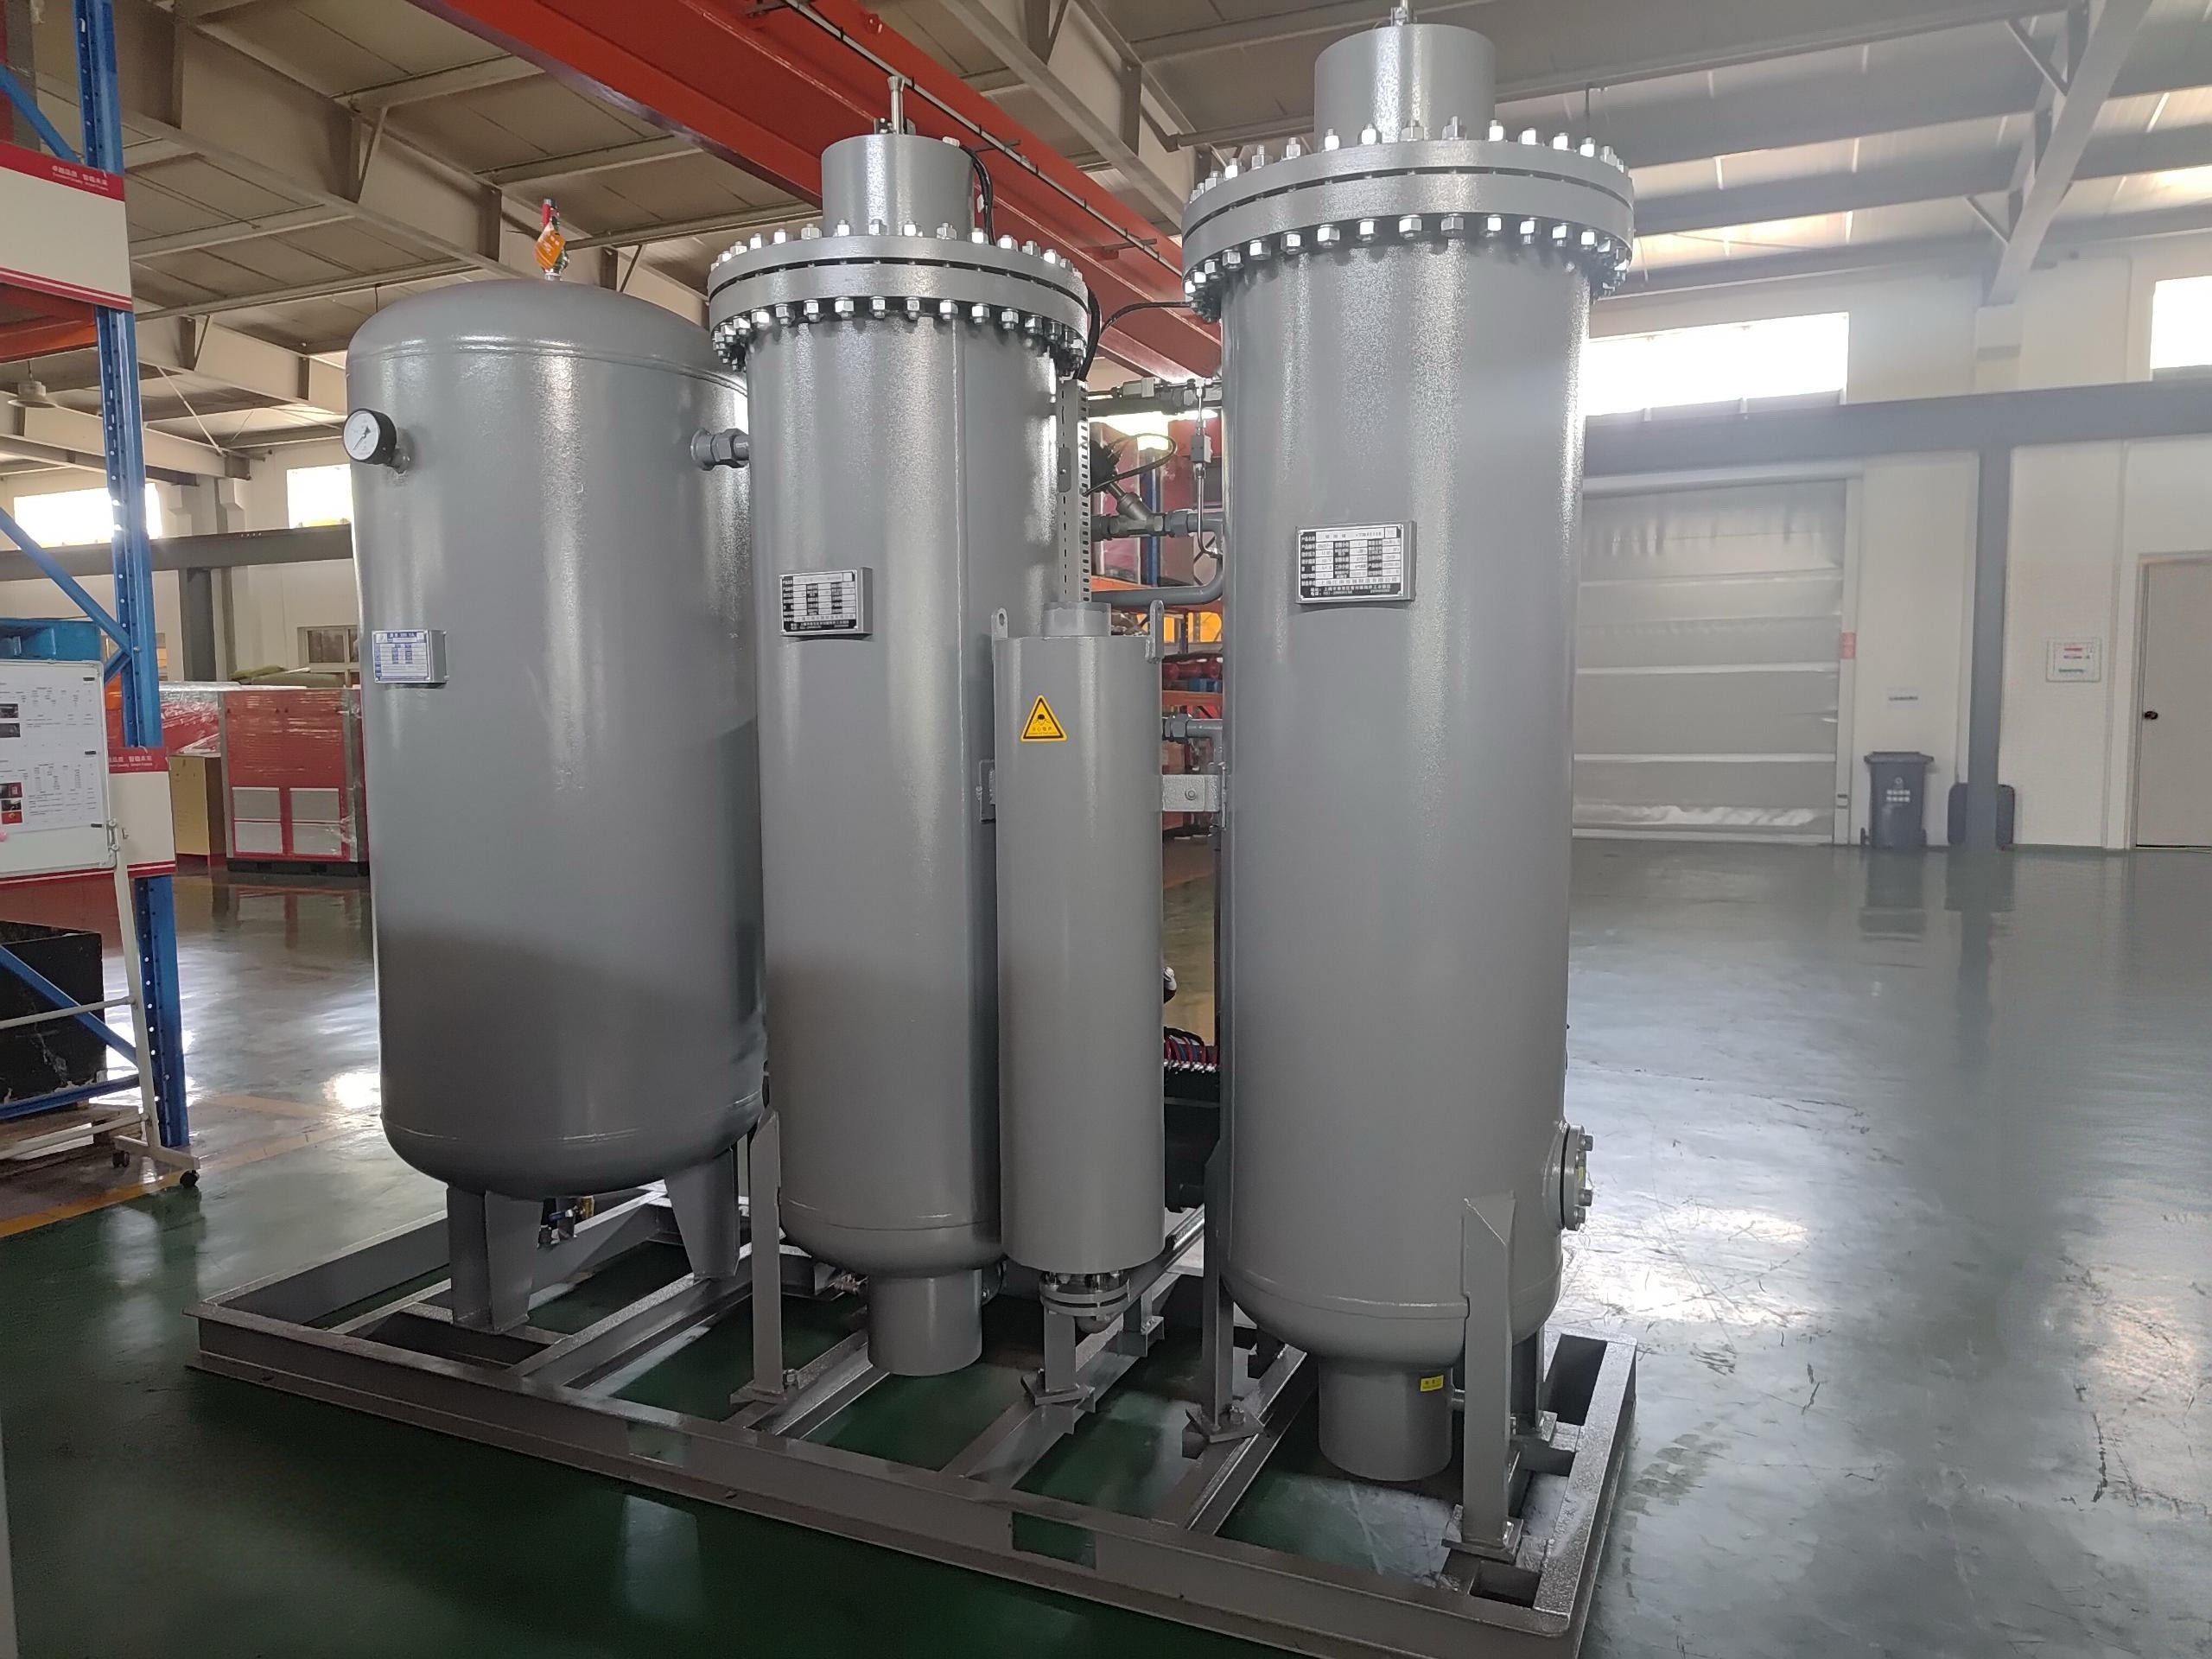
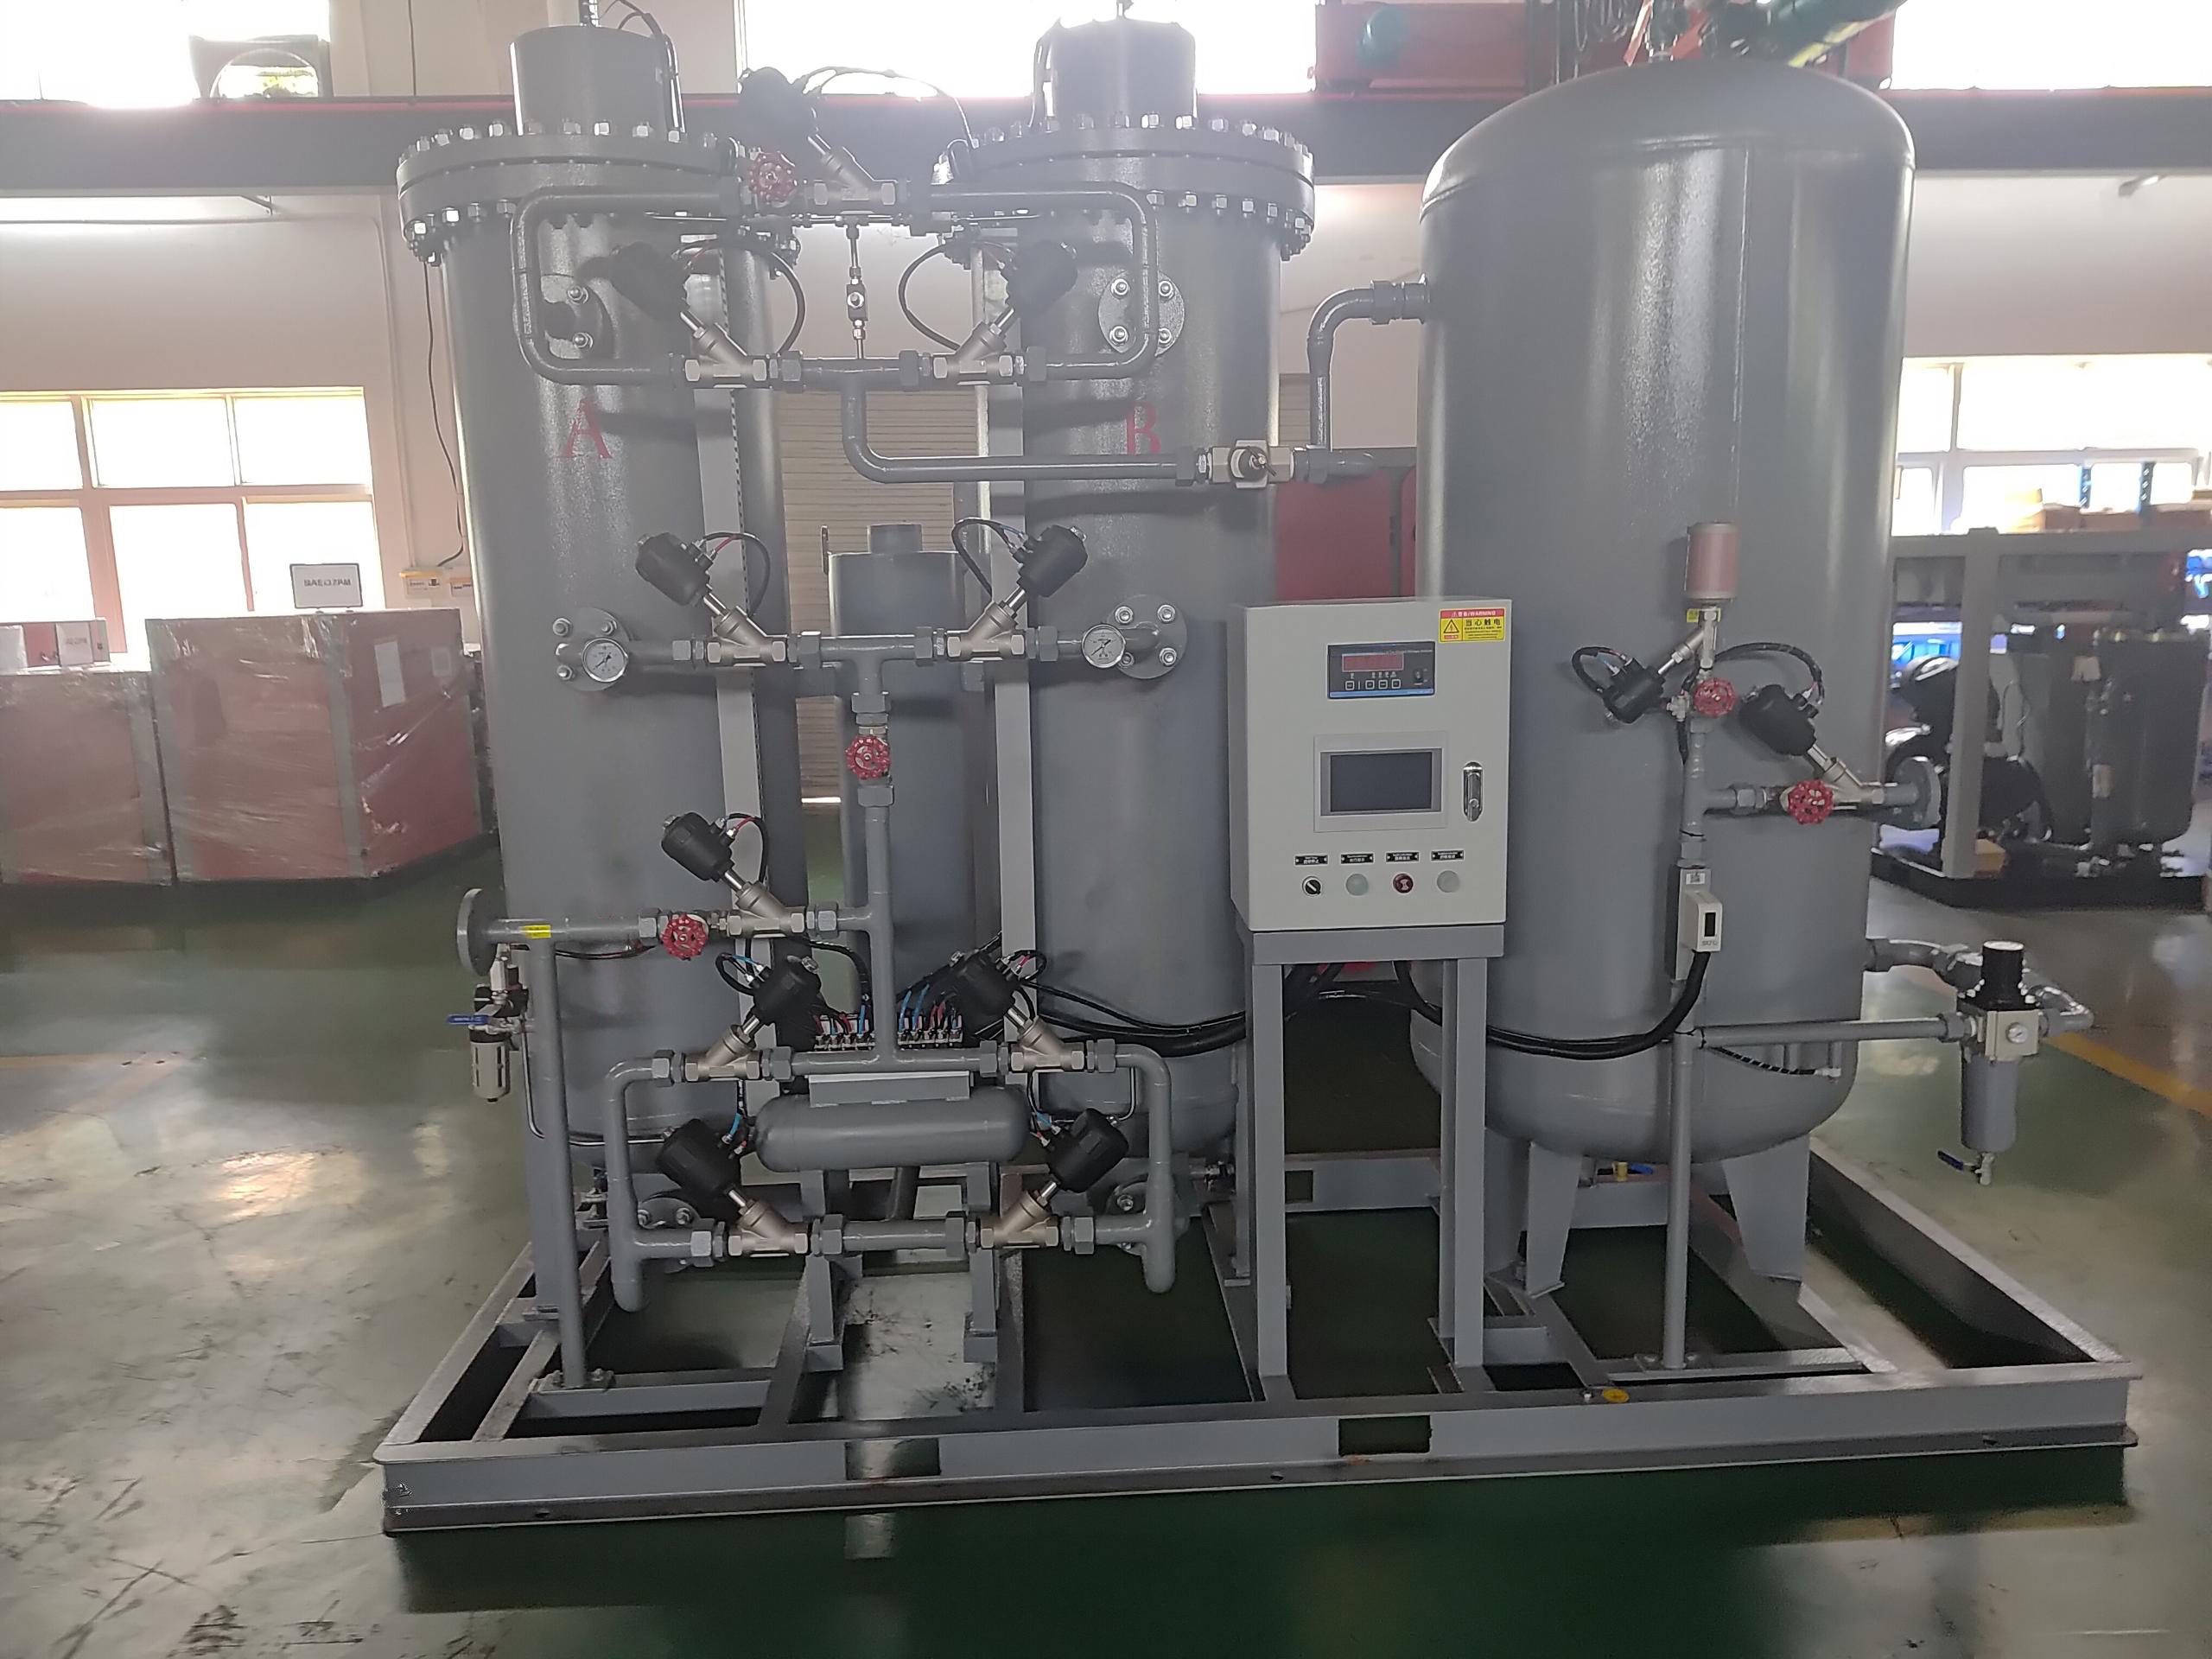
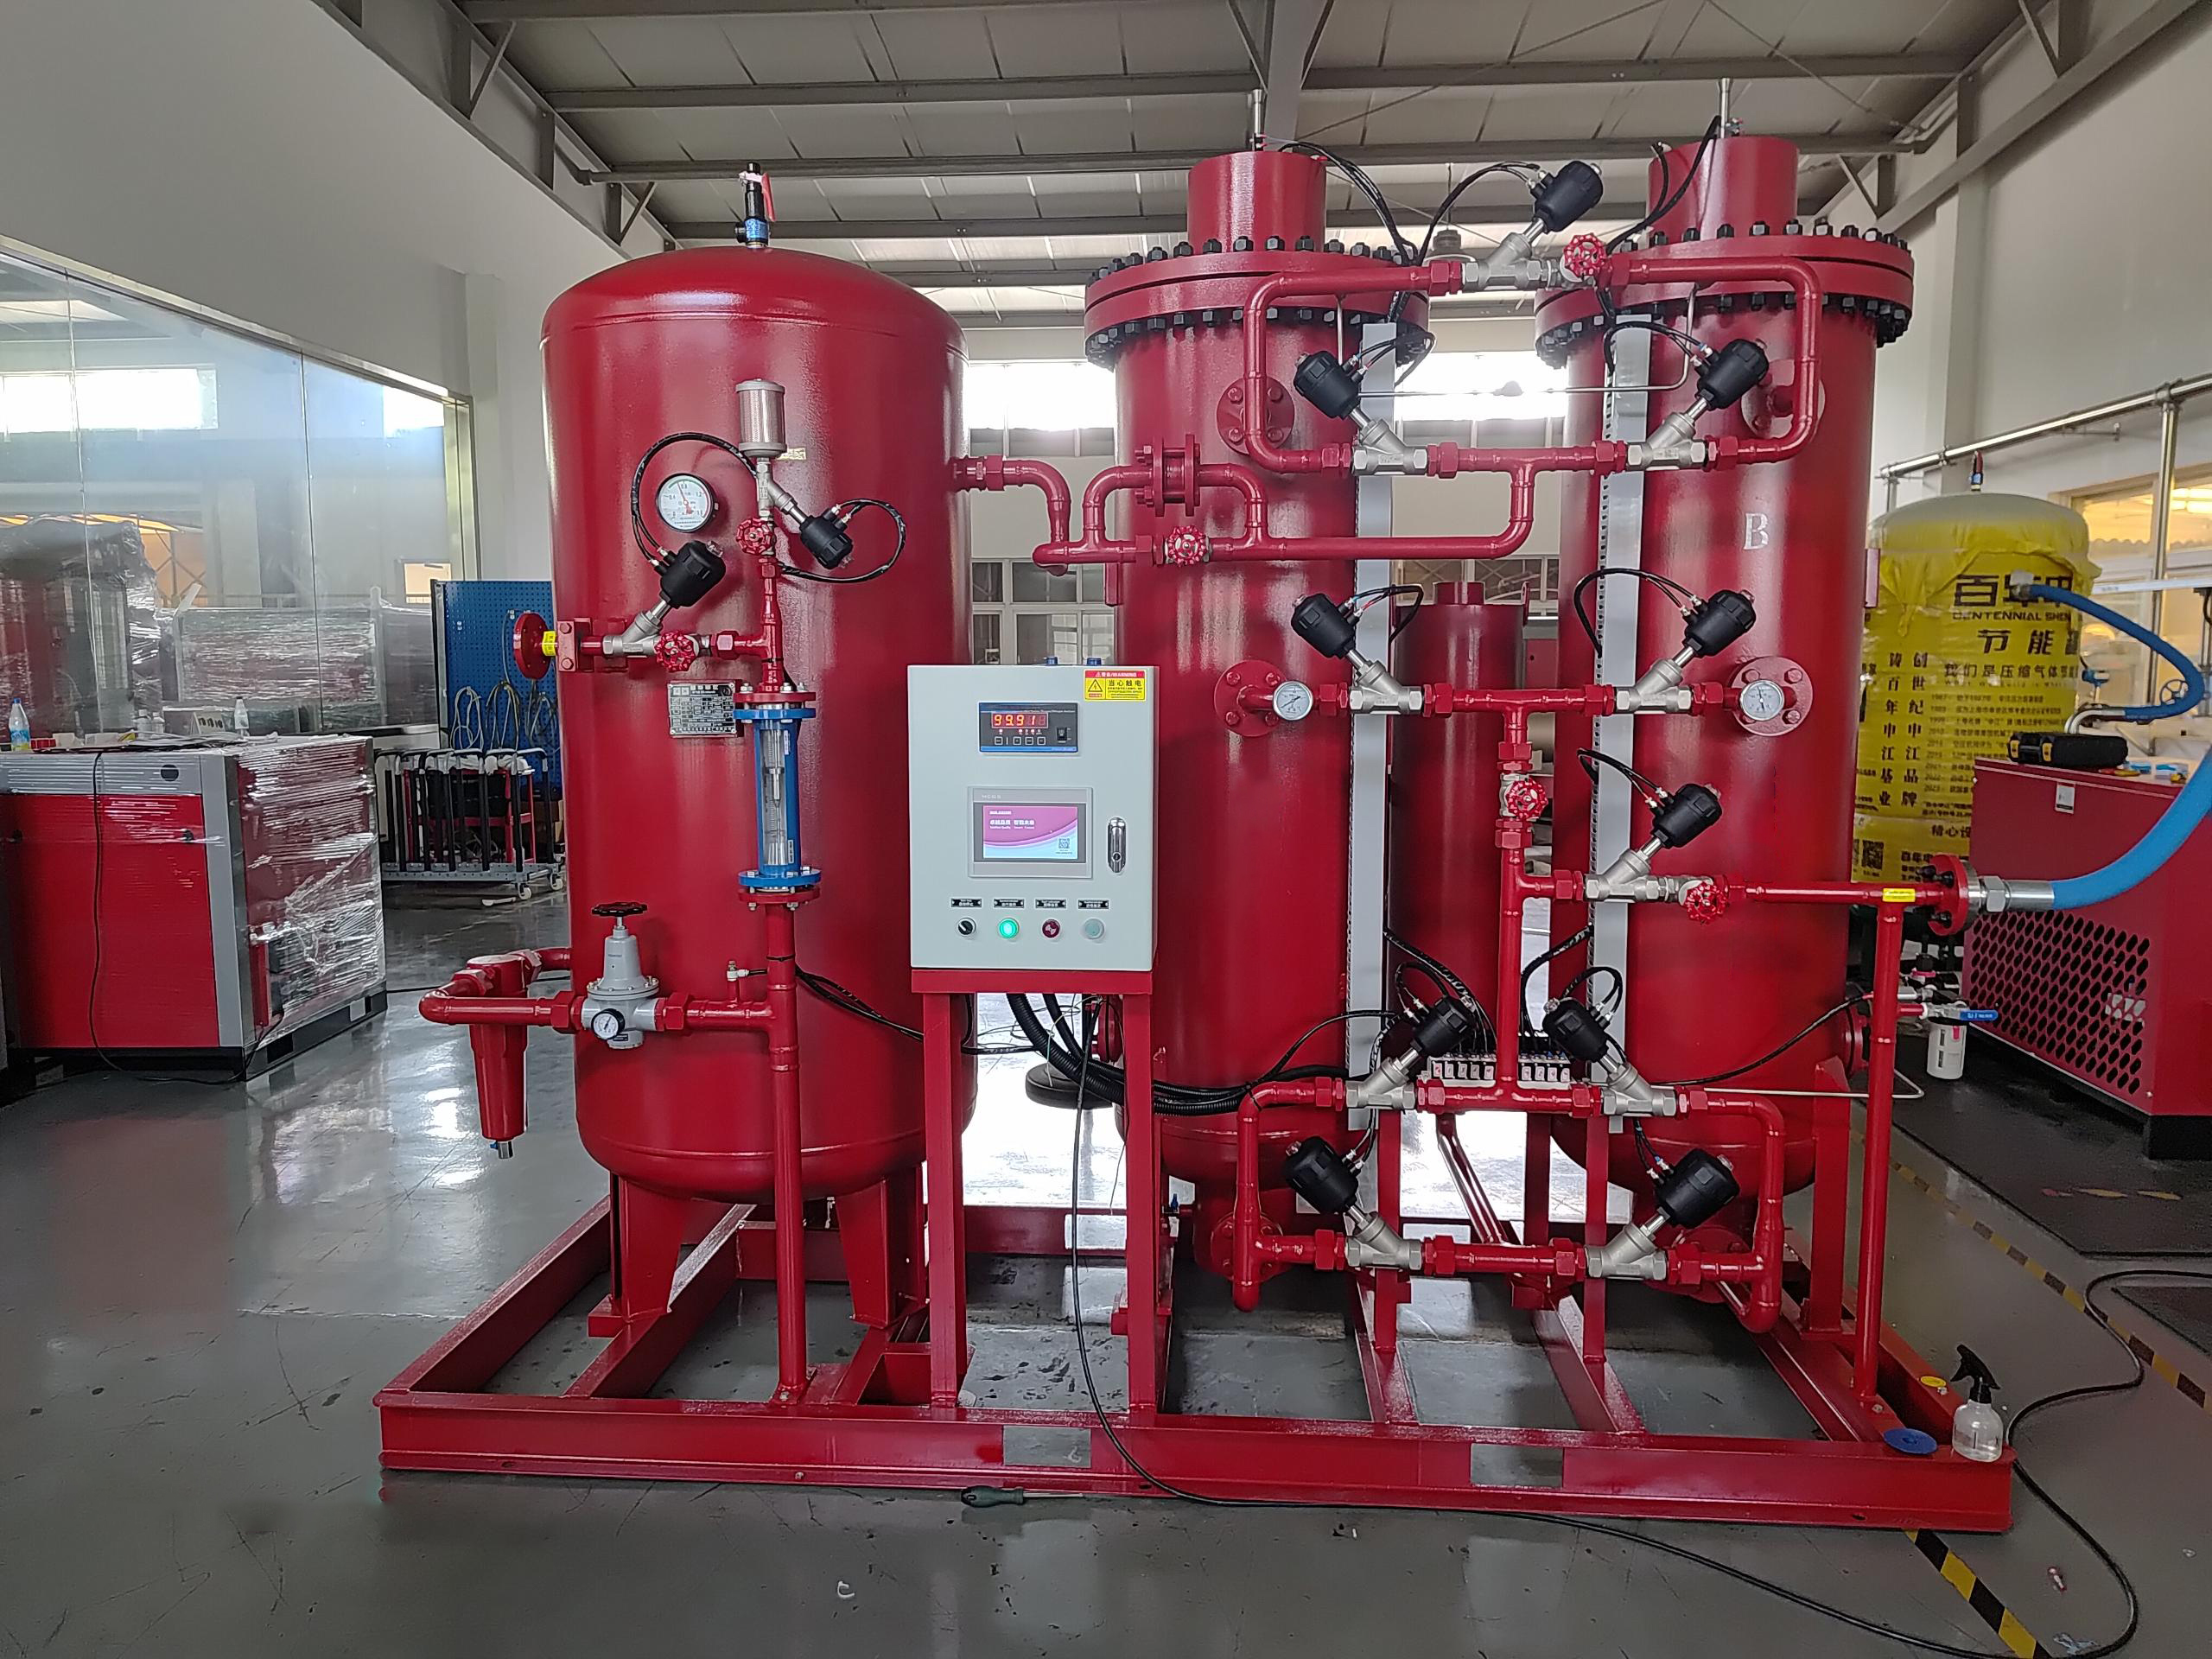
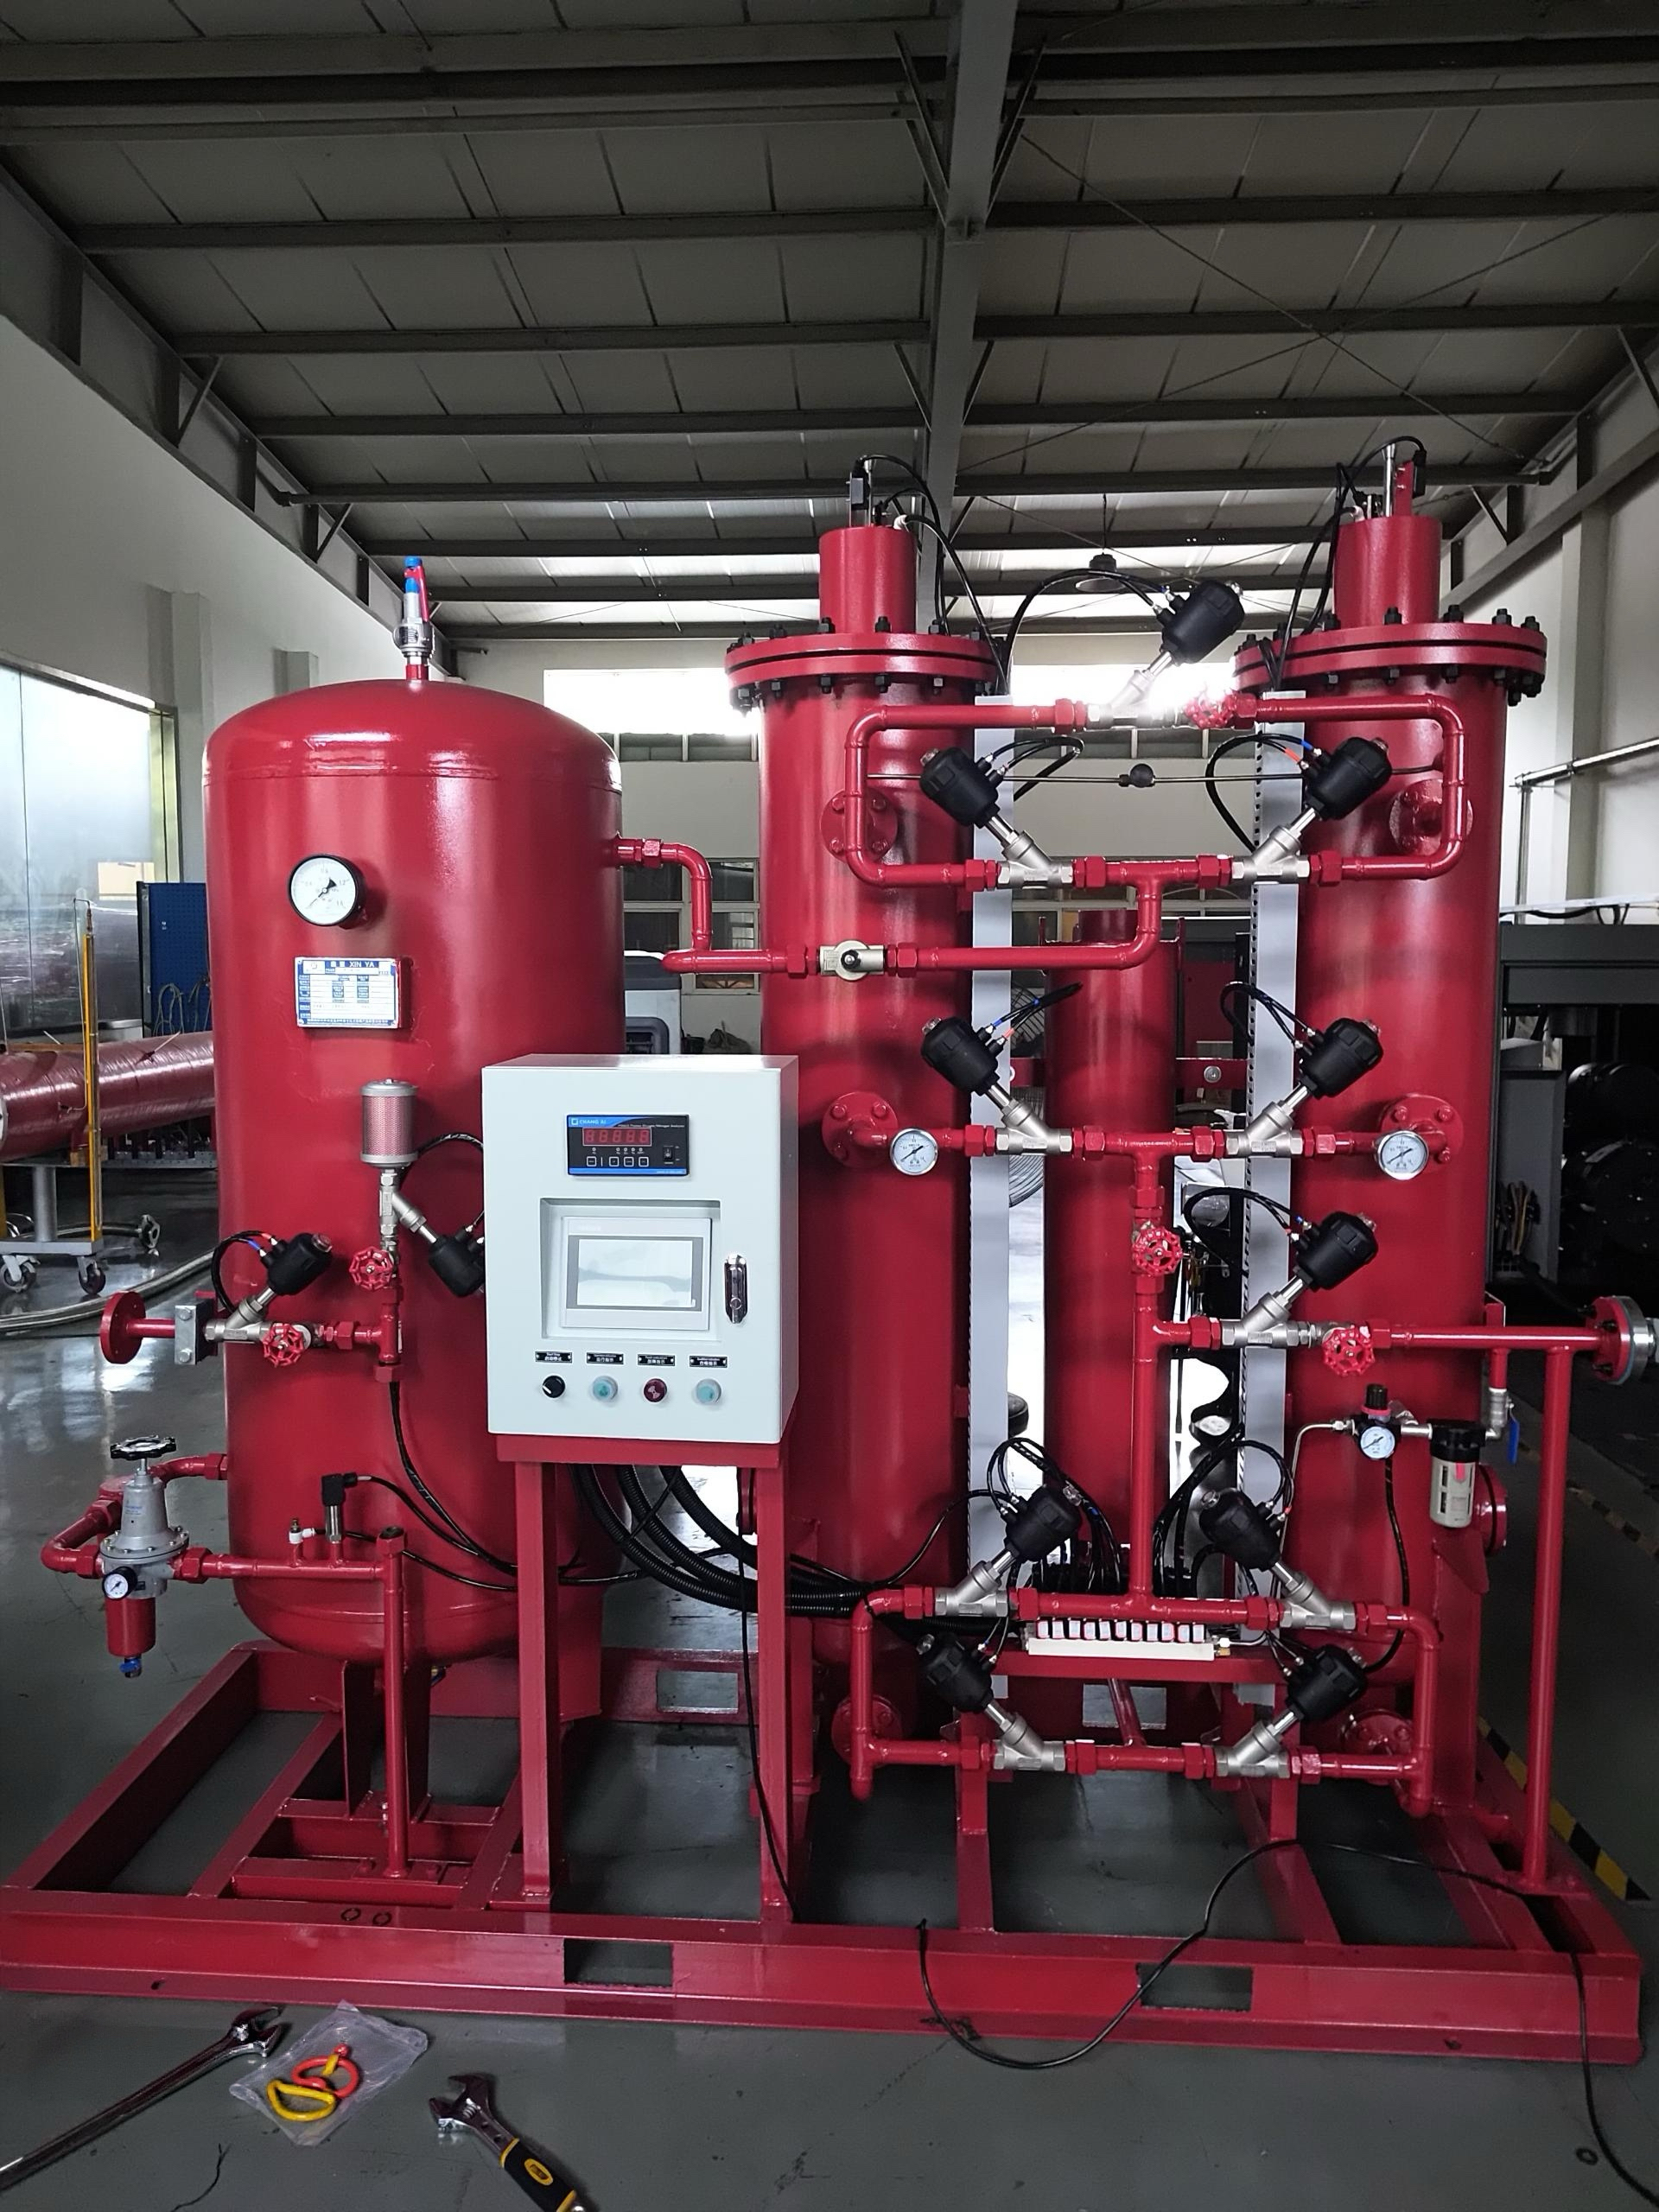
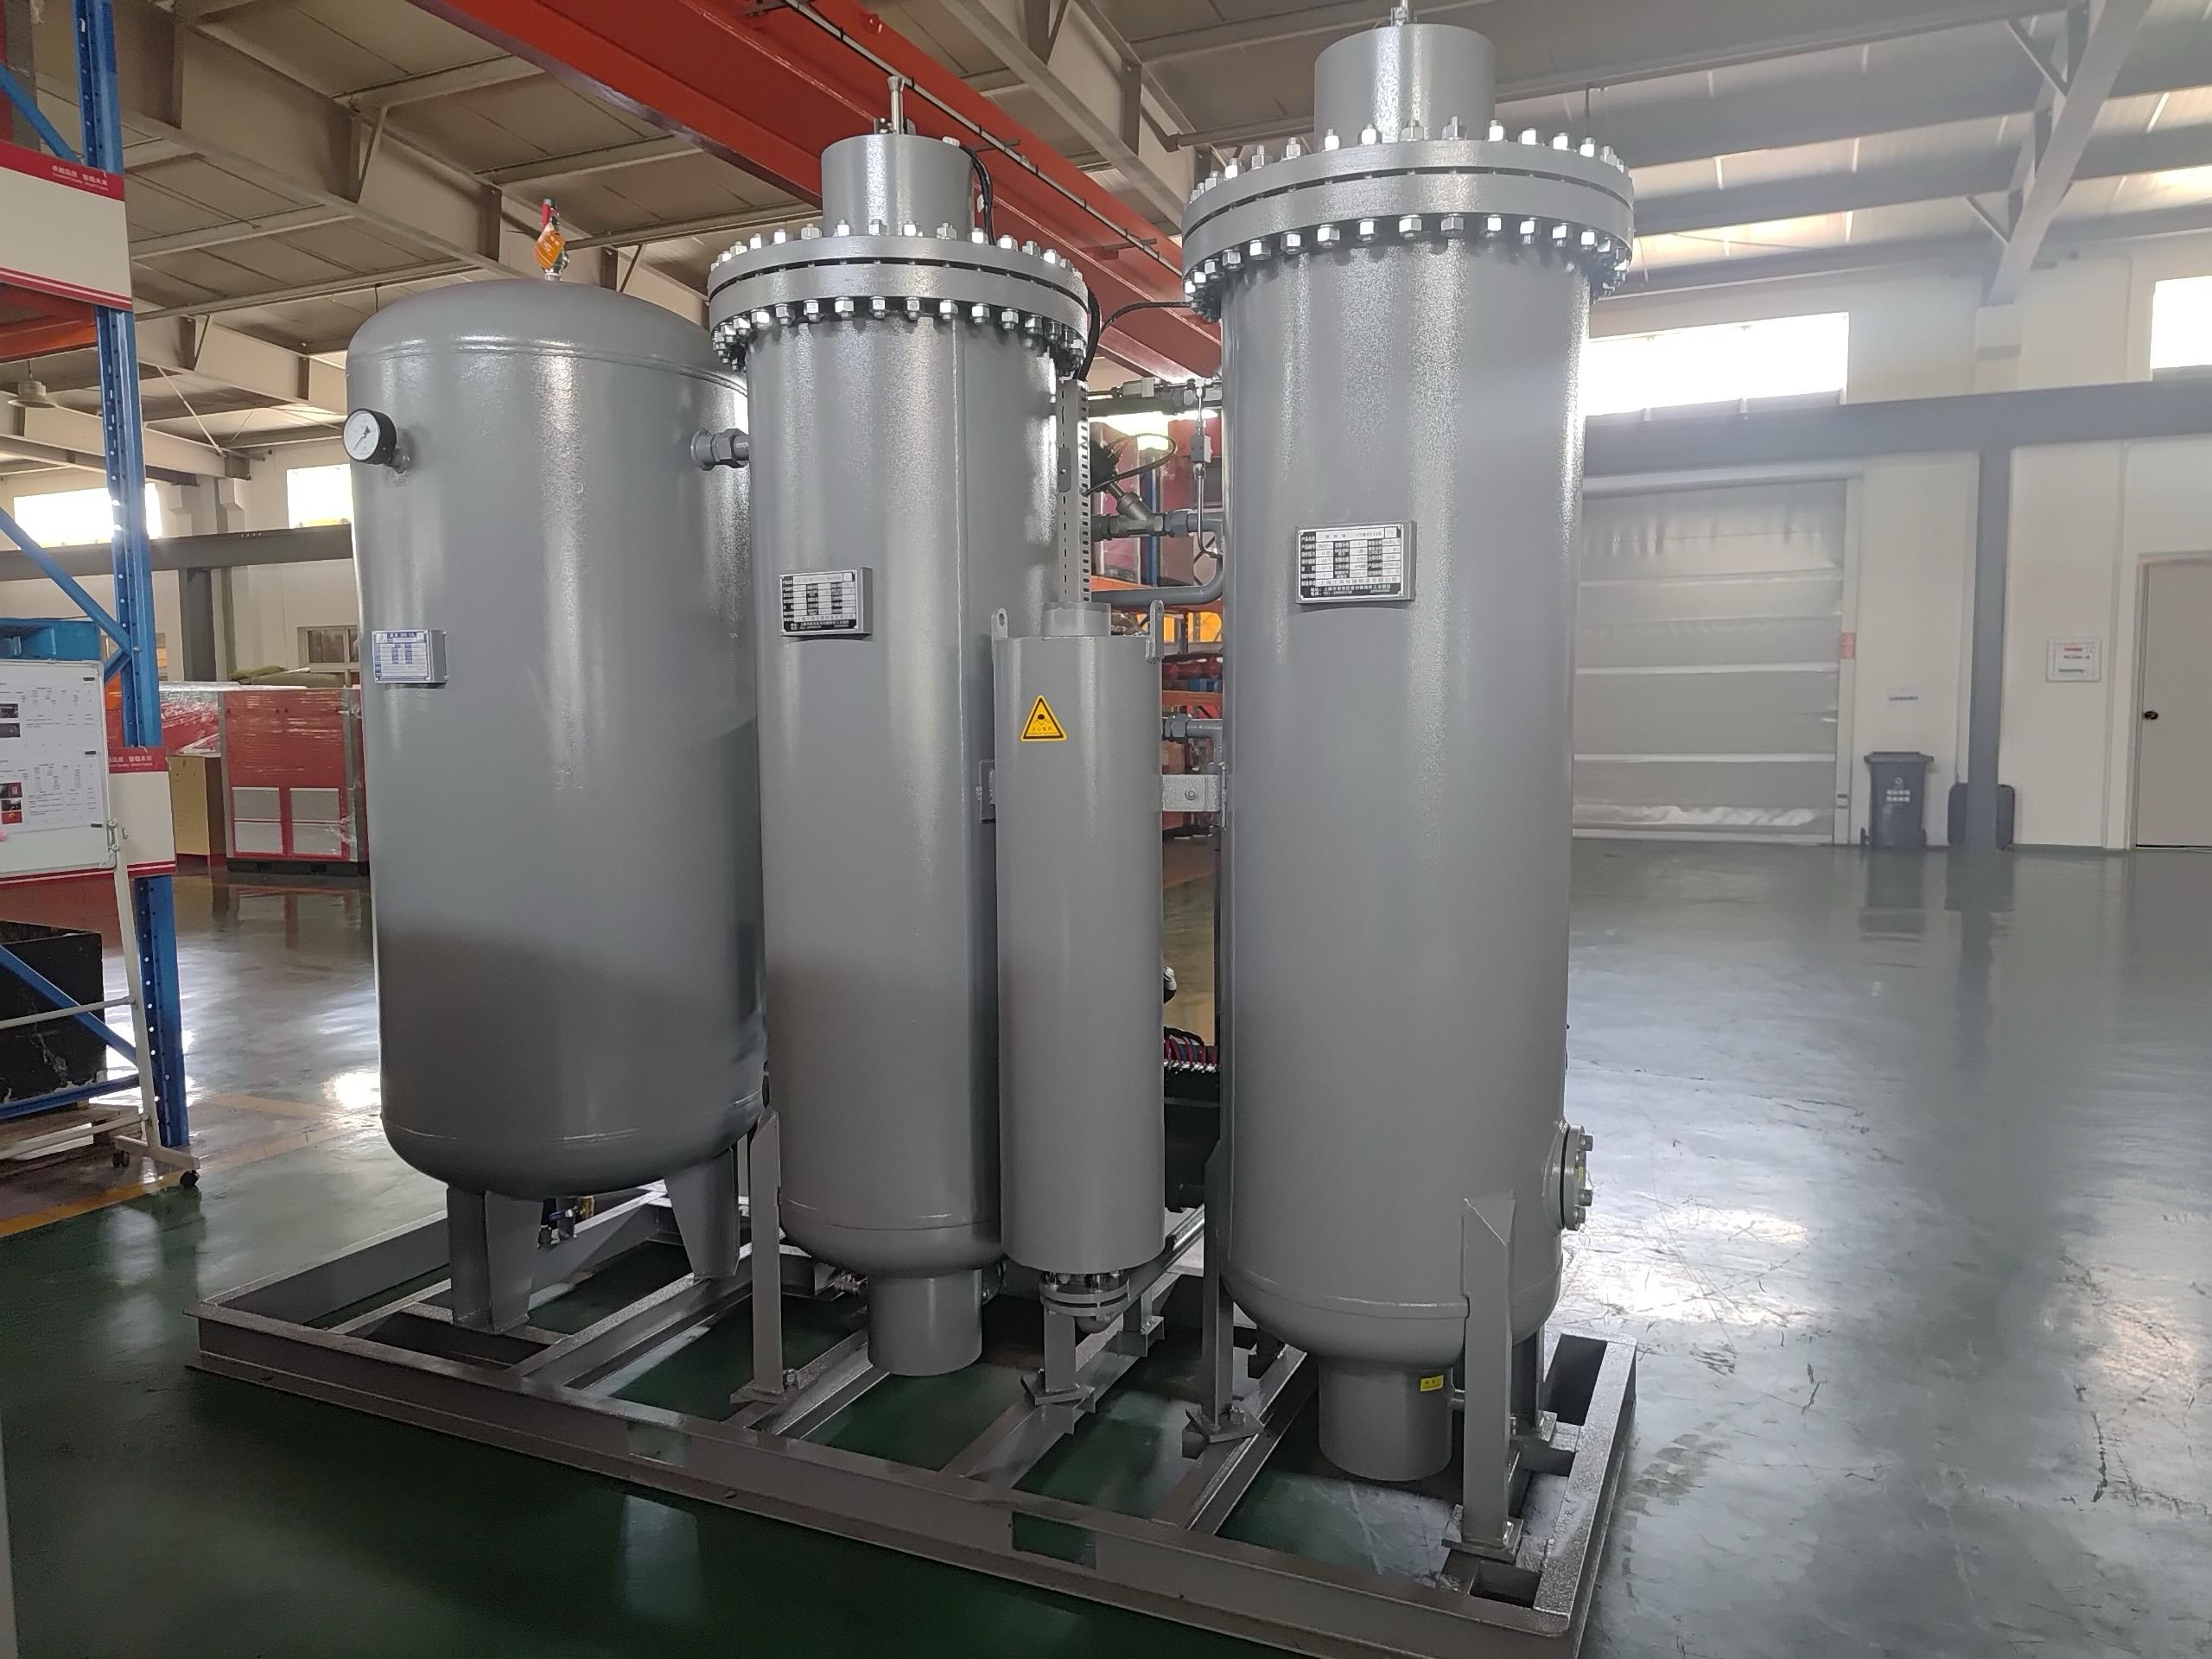
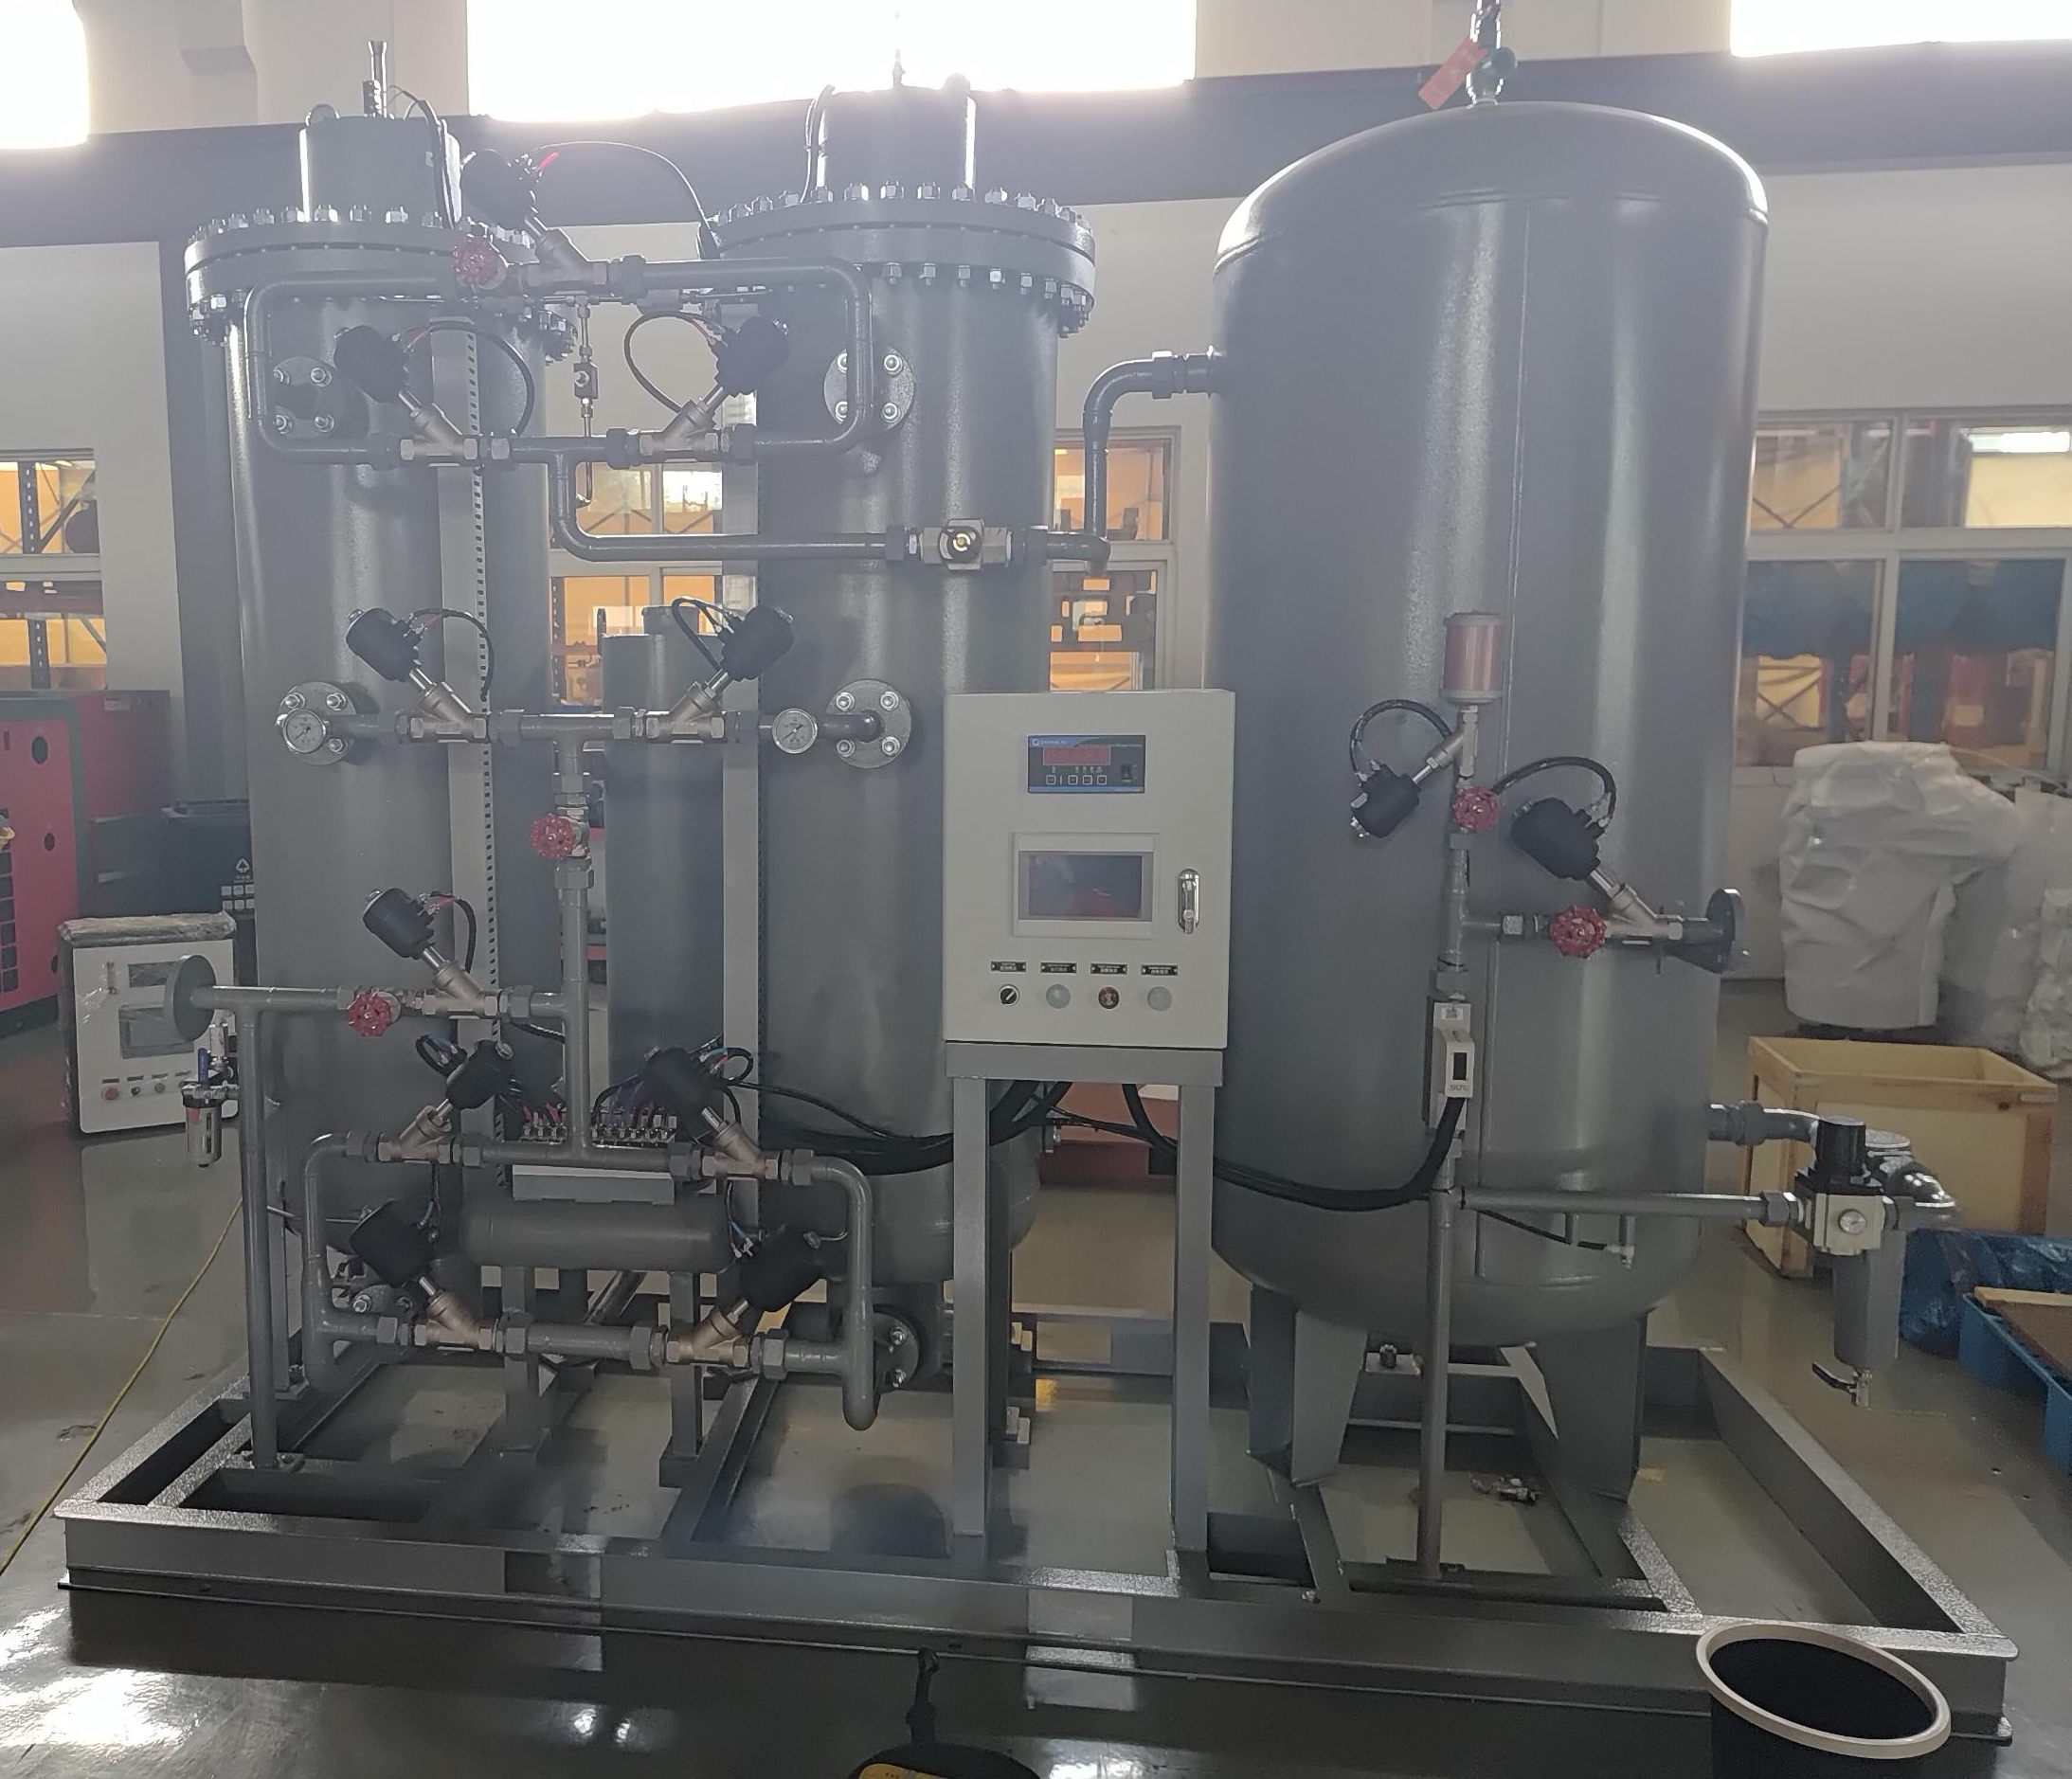
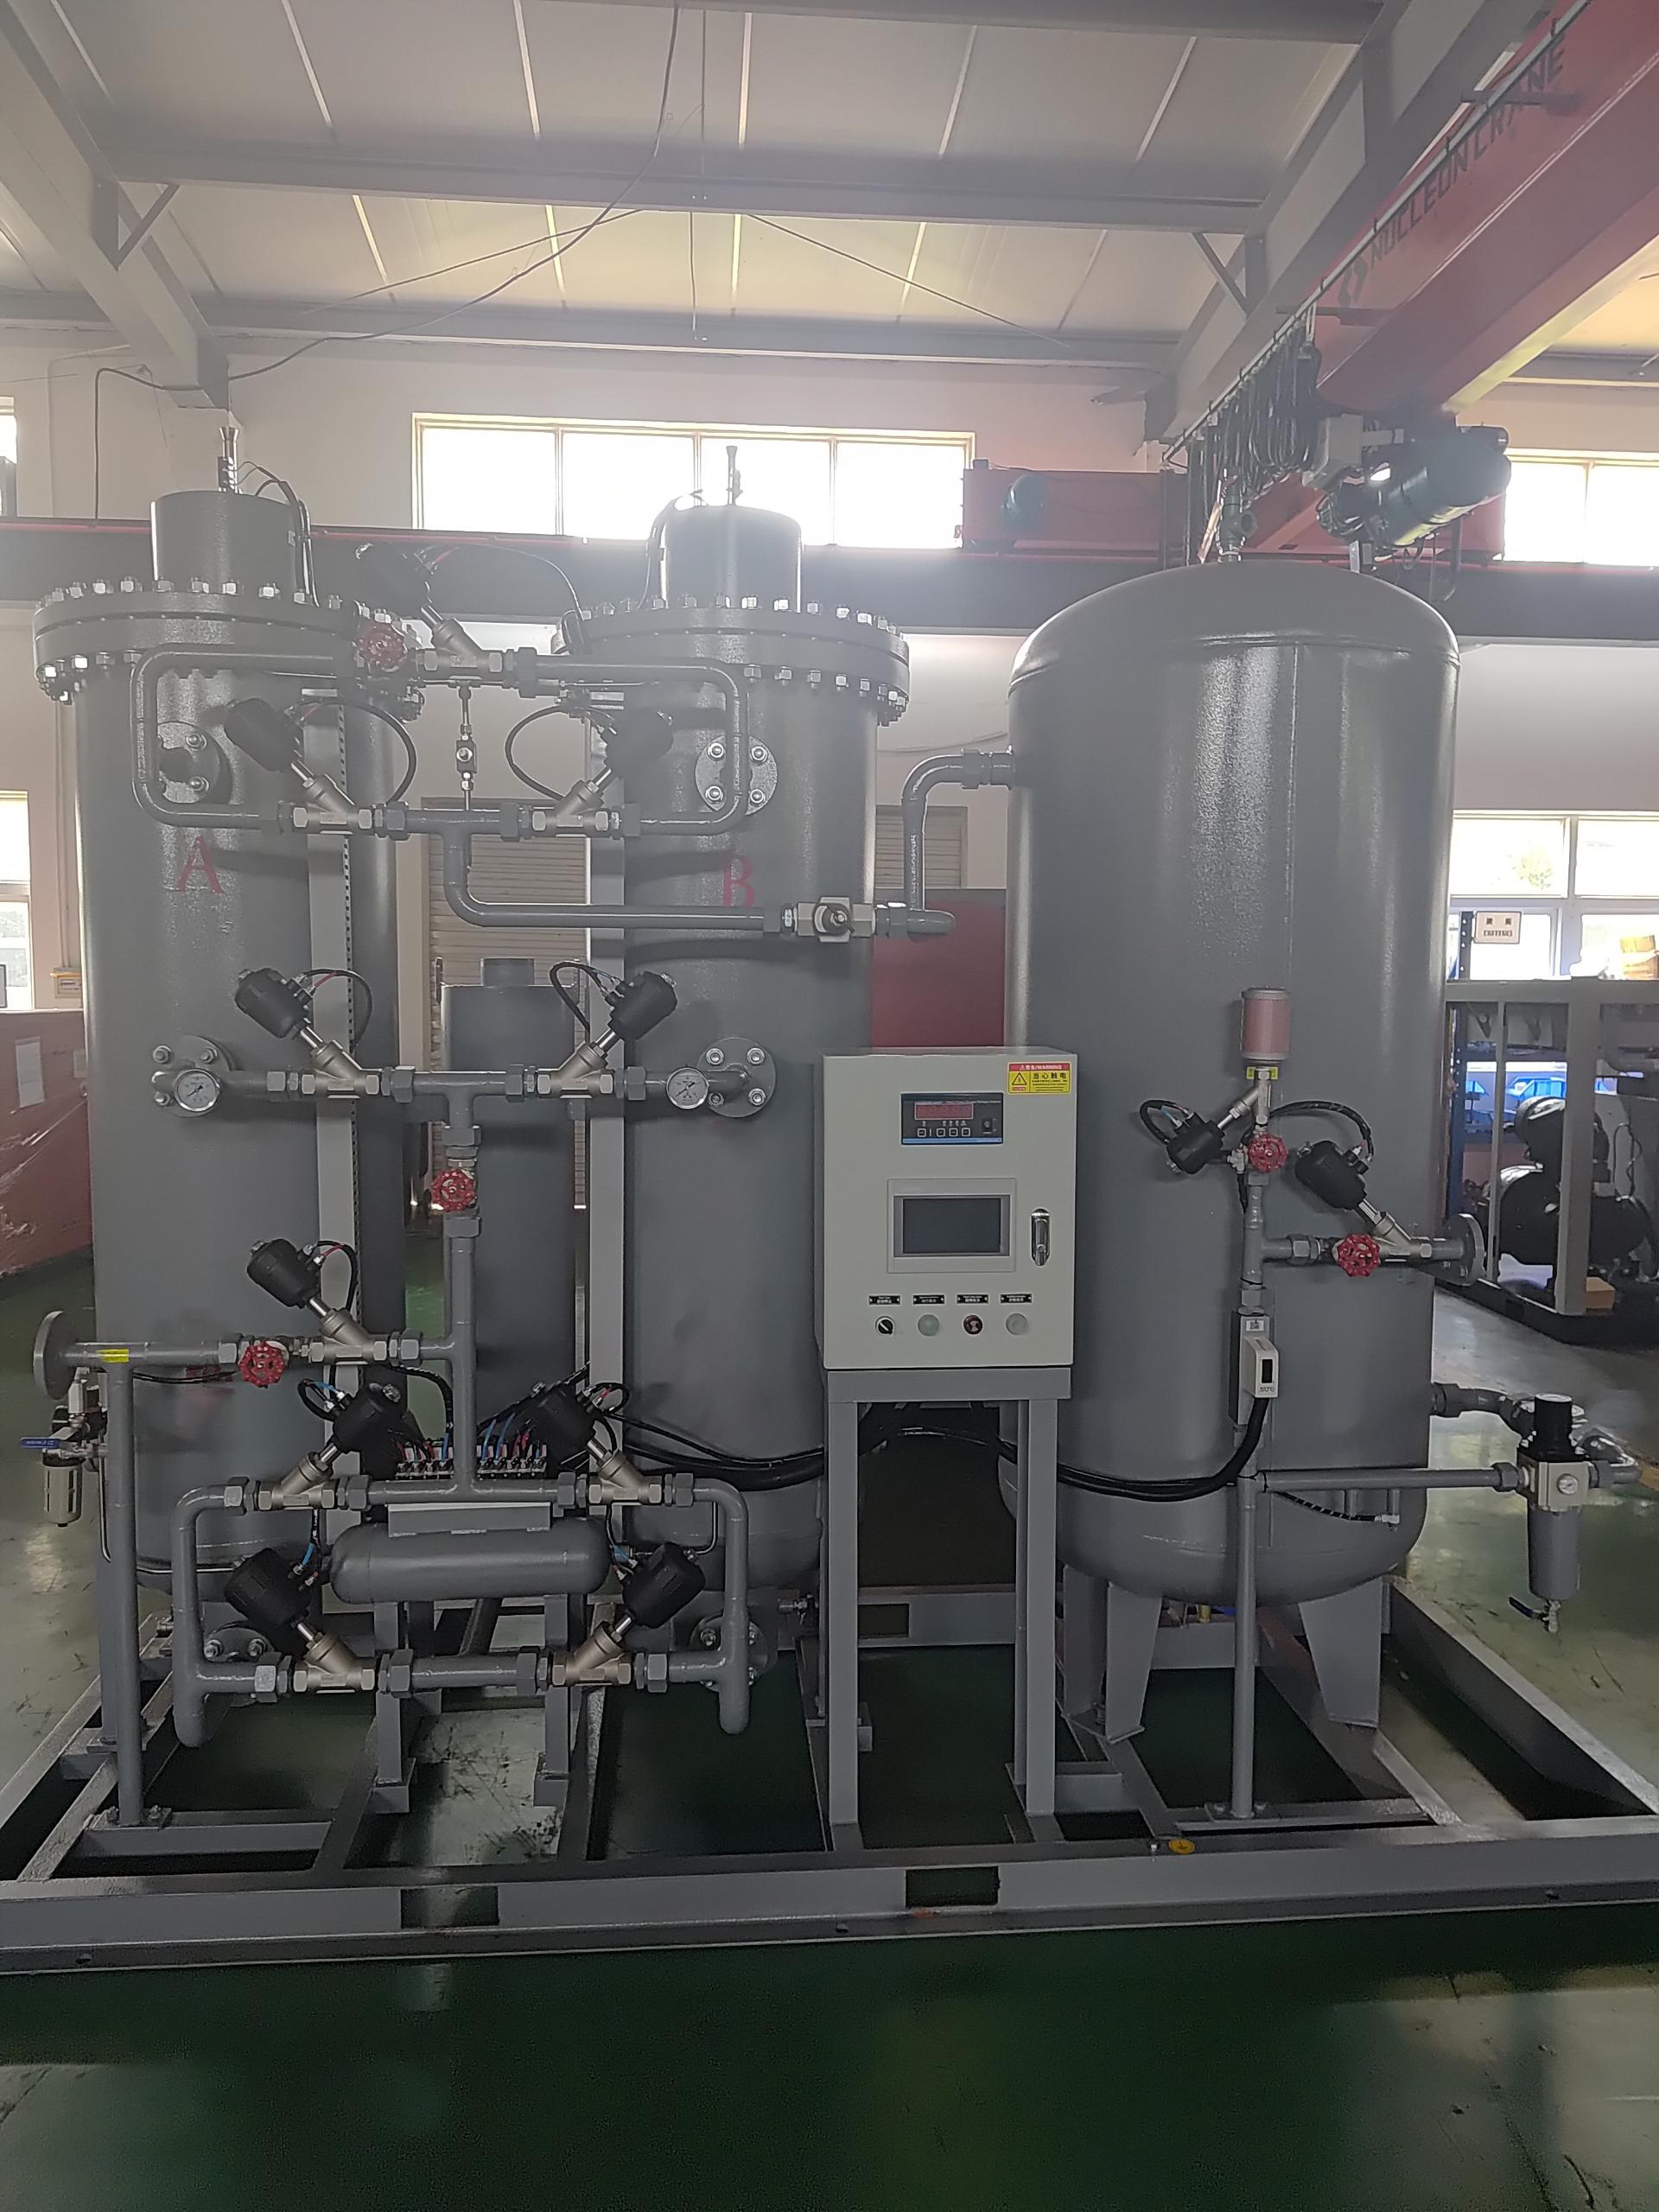
Product Description
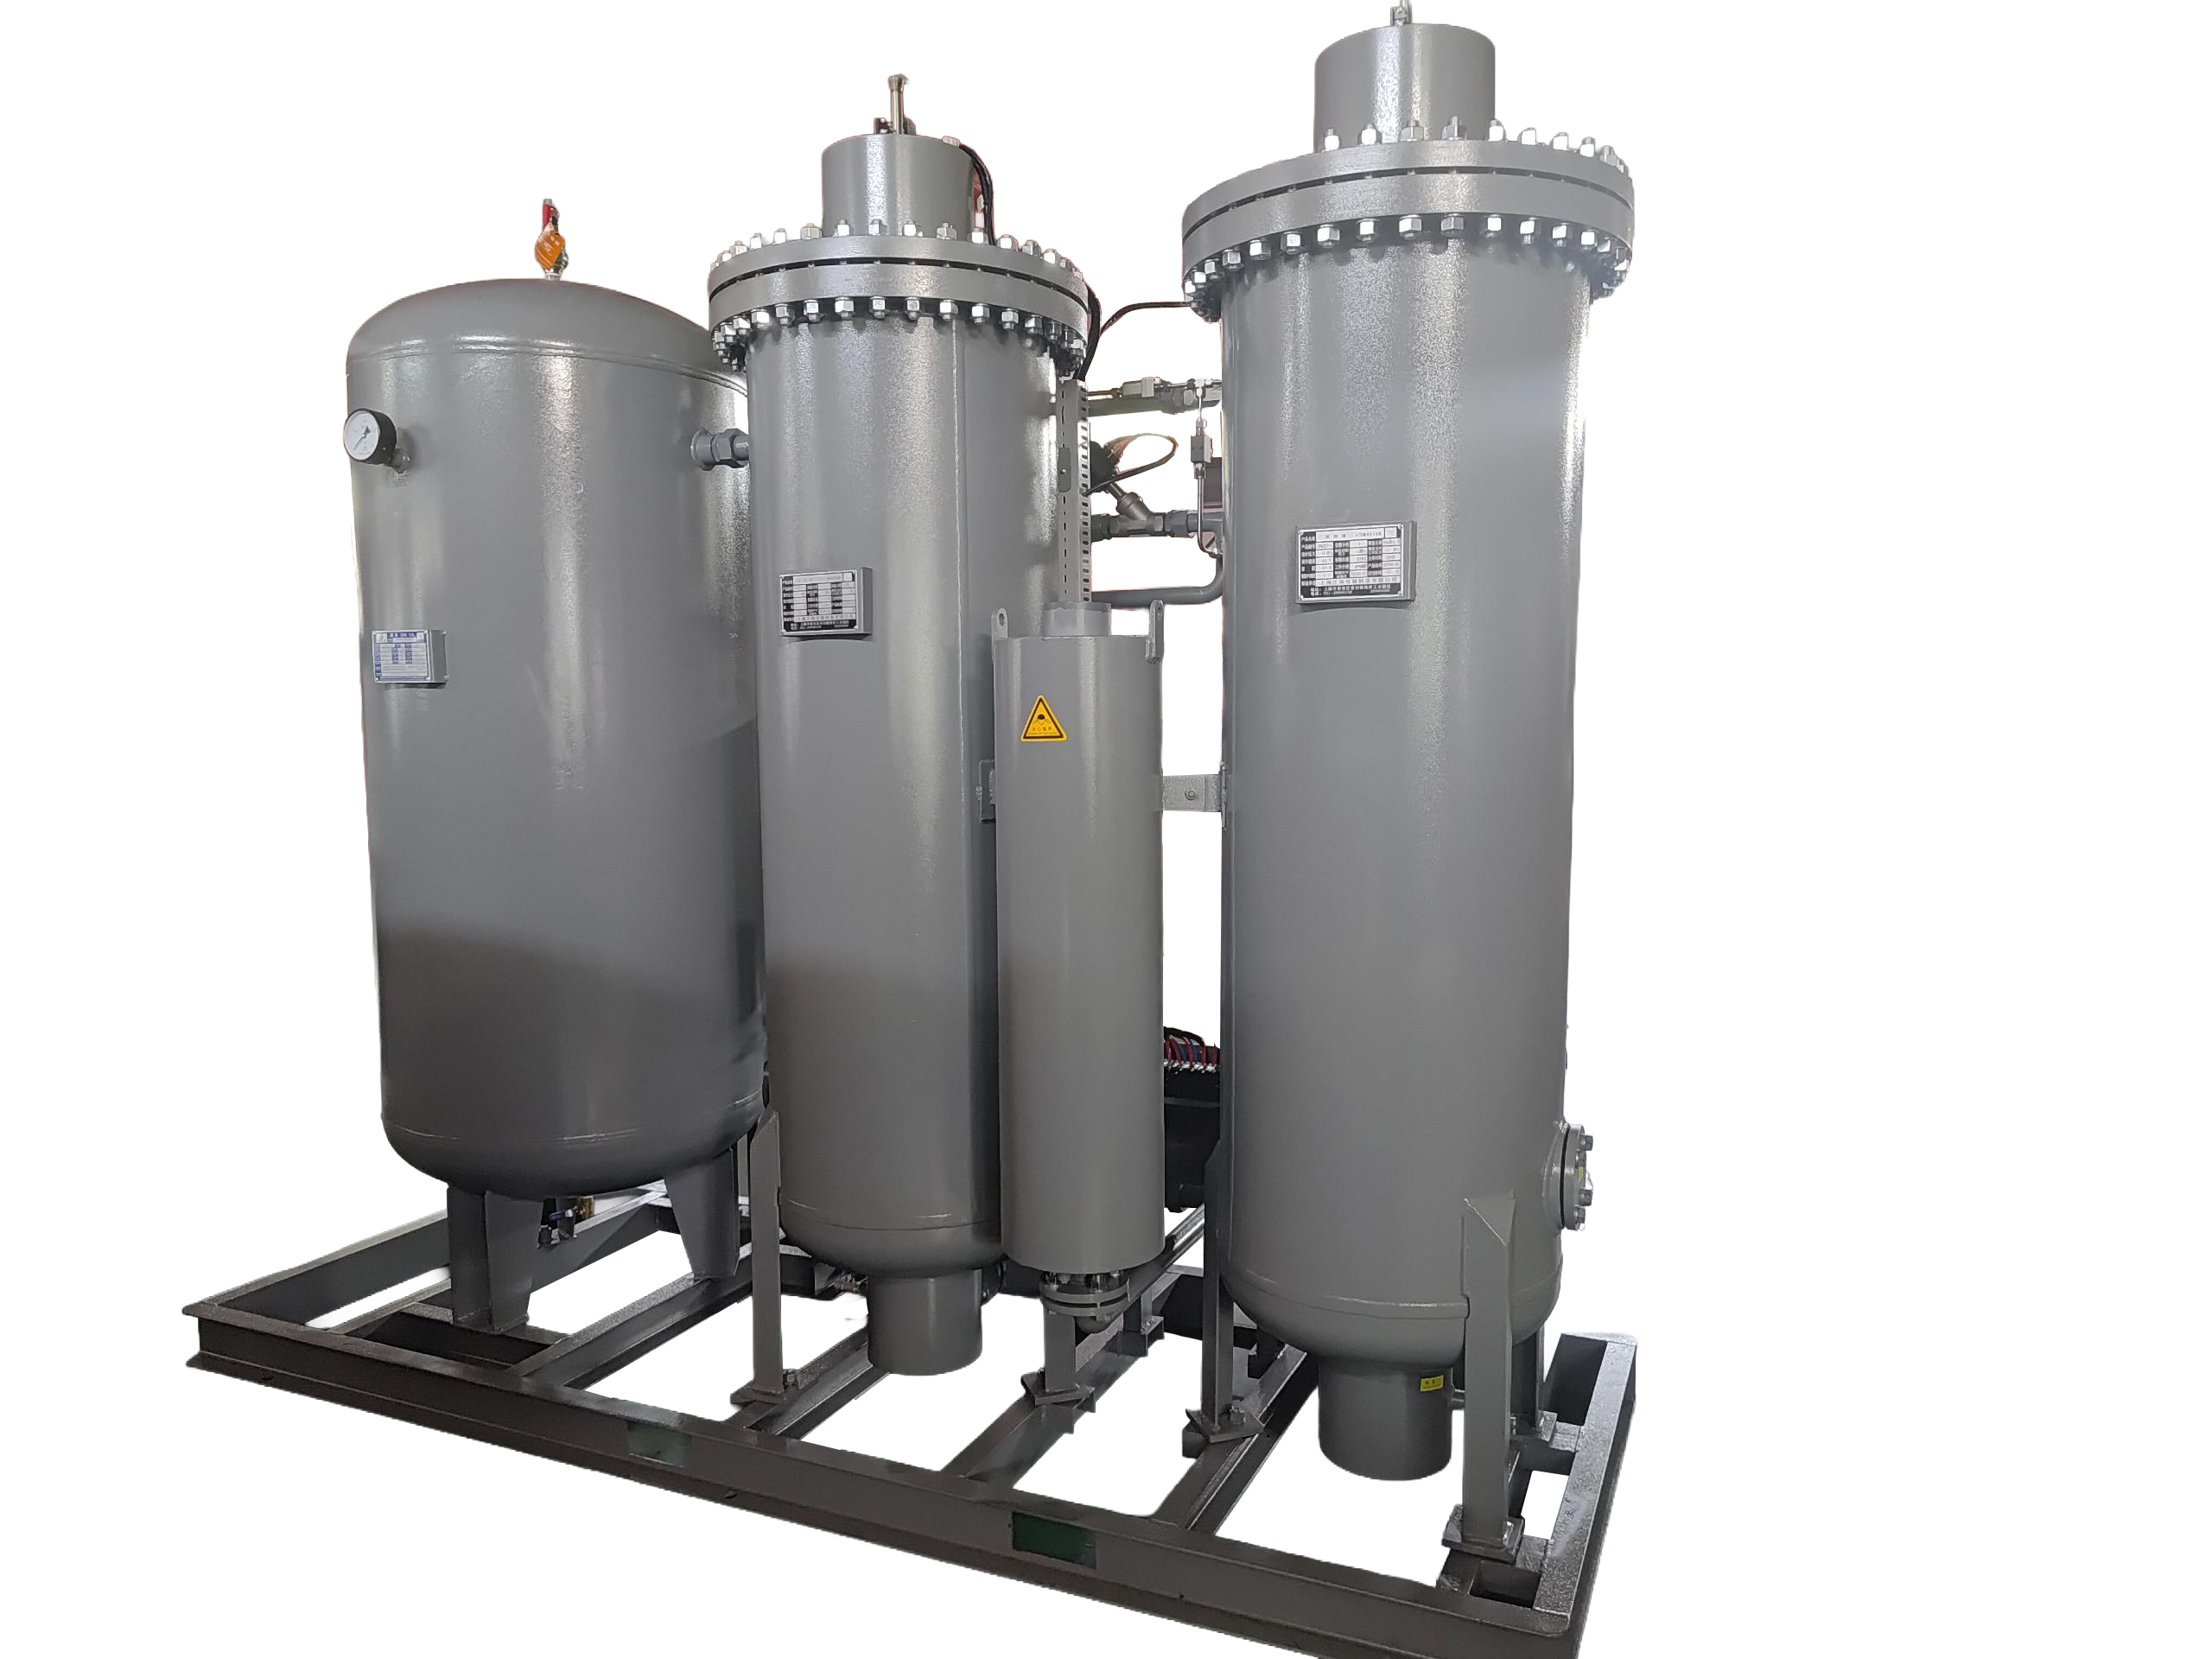
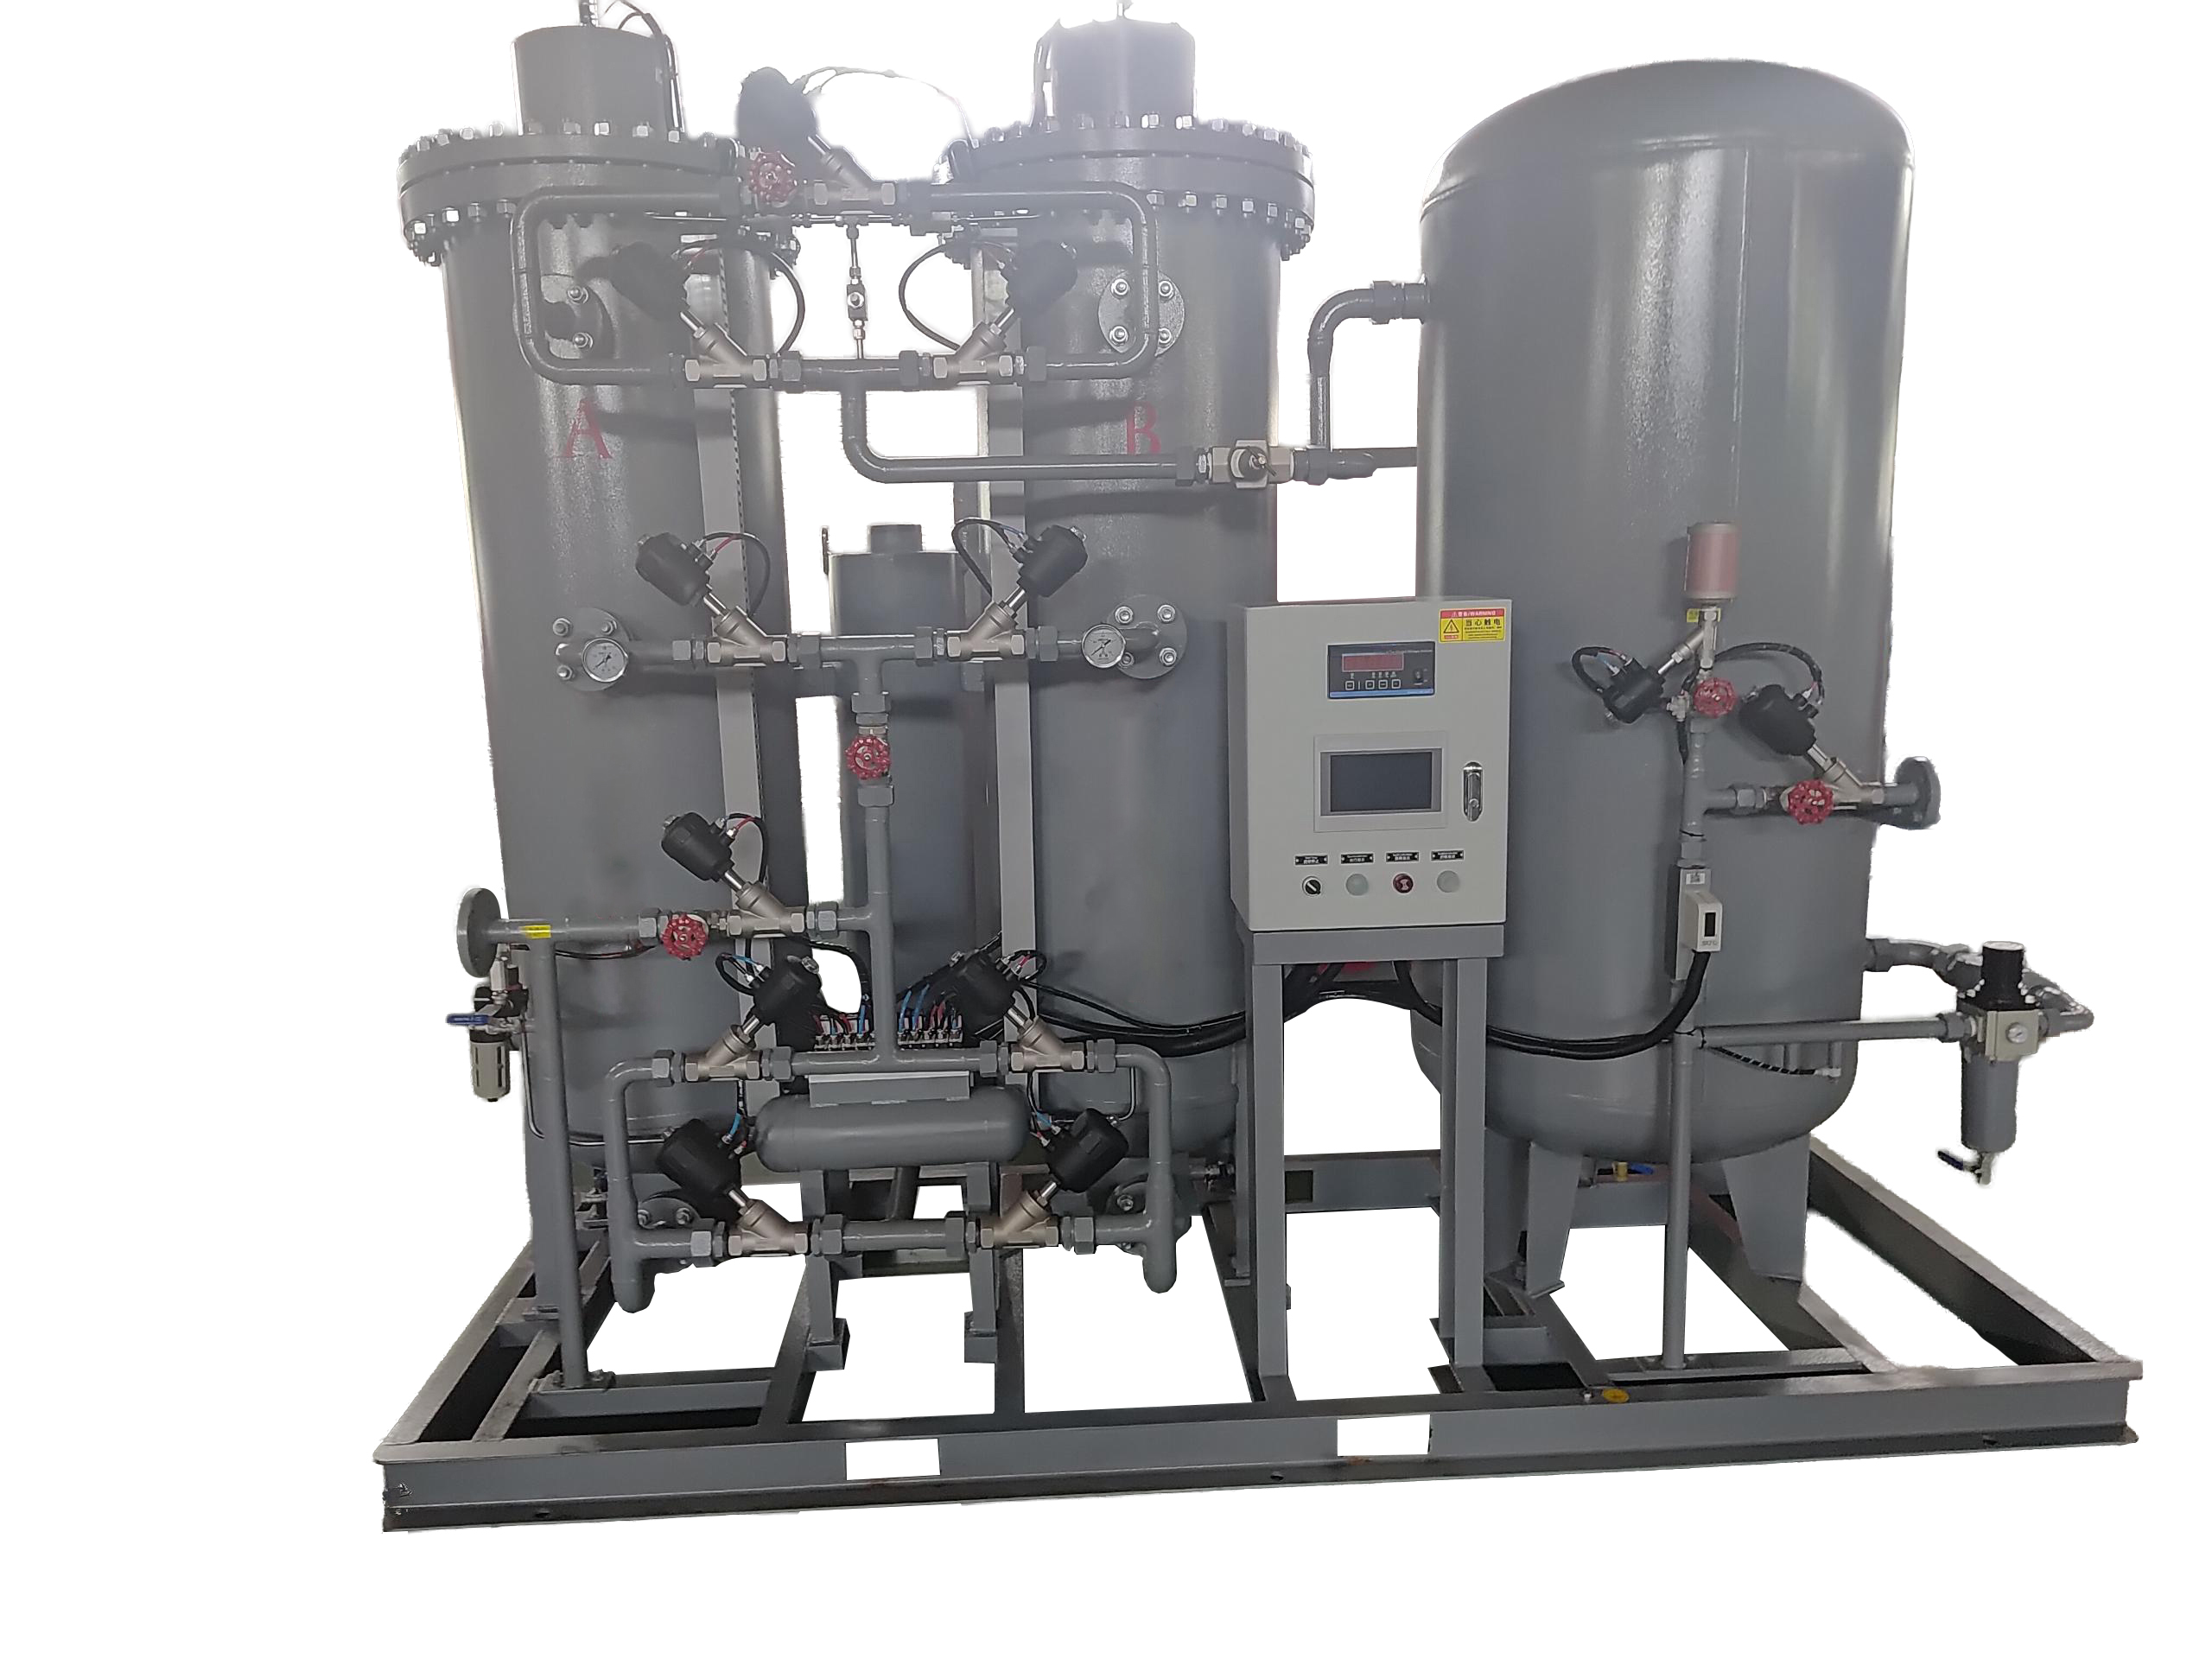
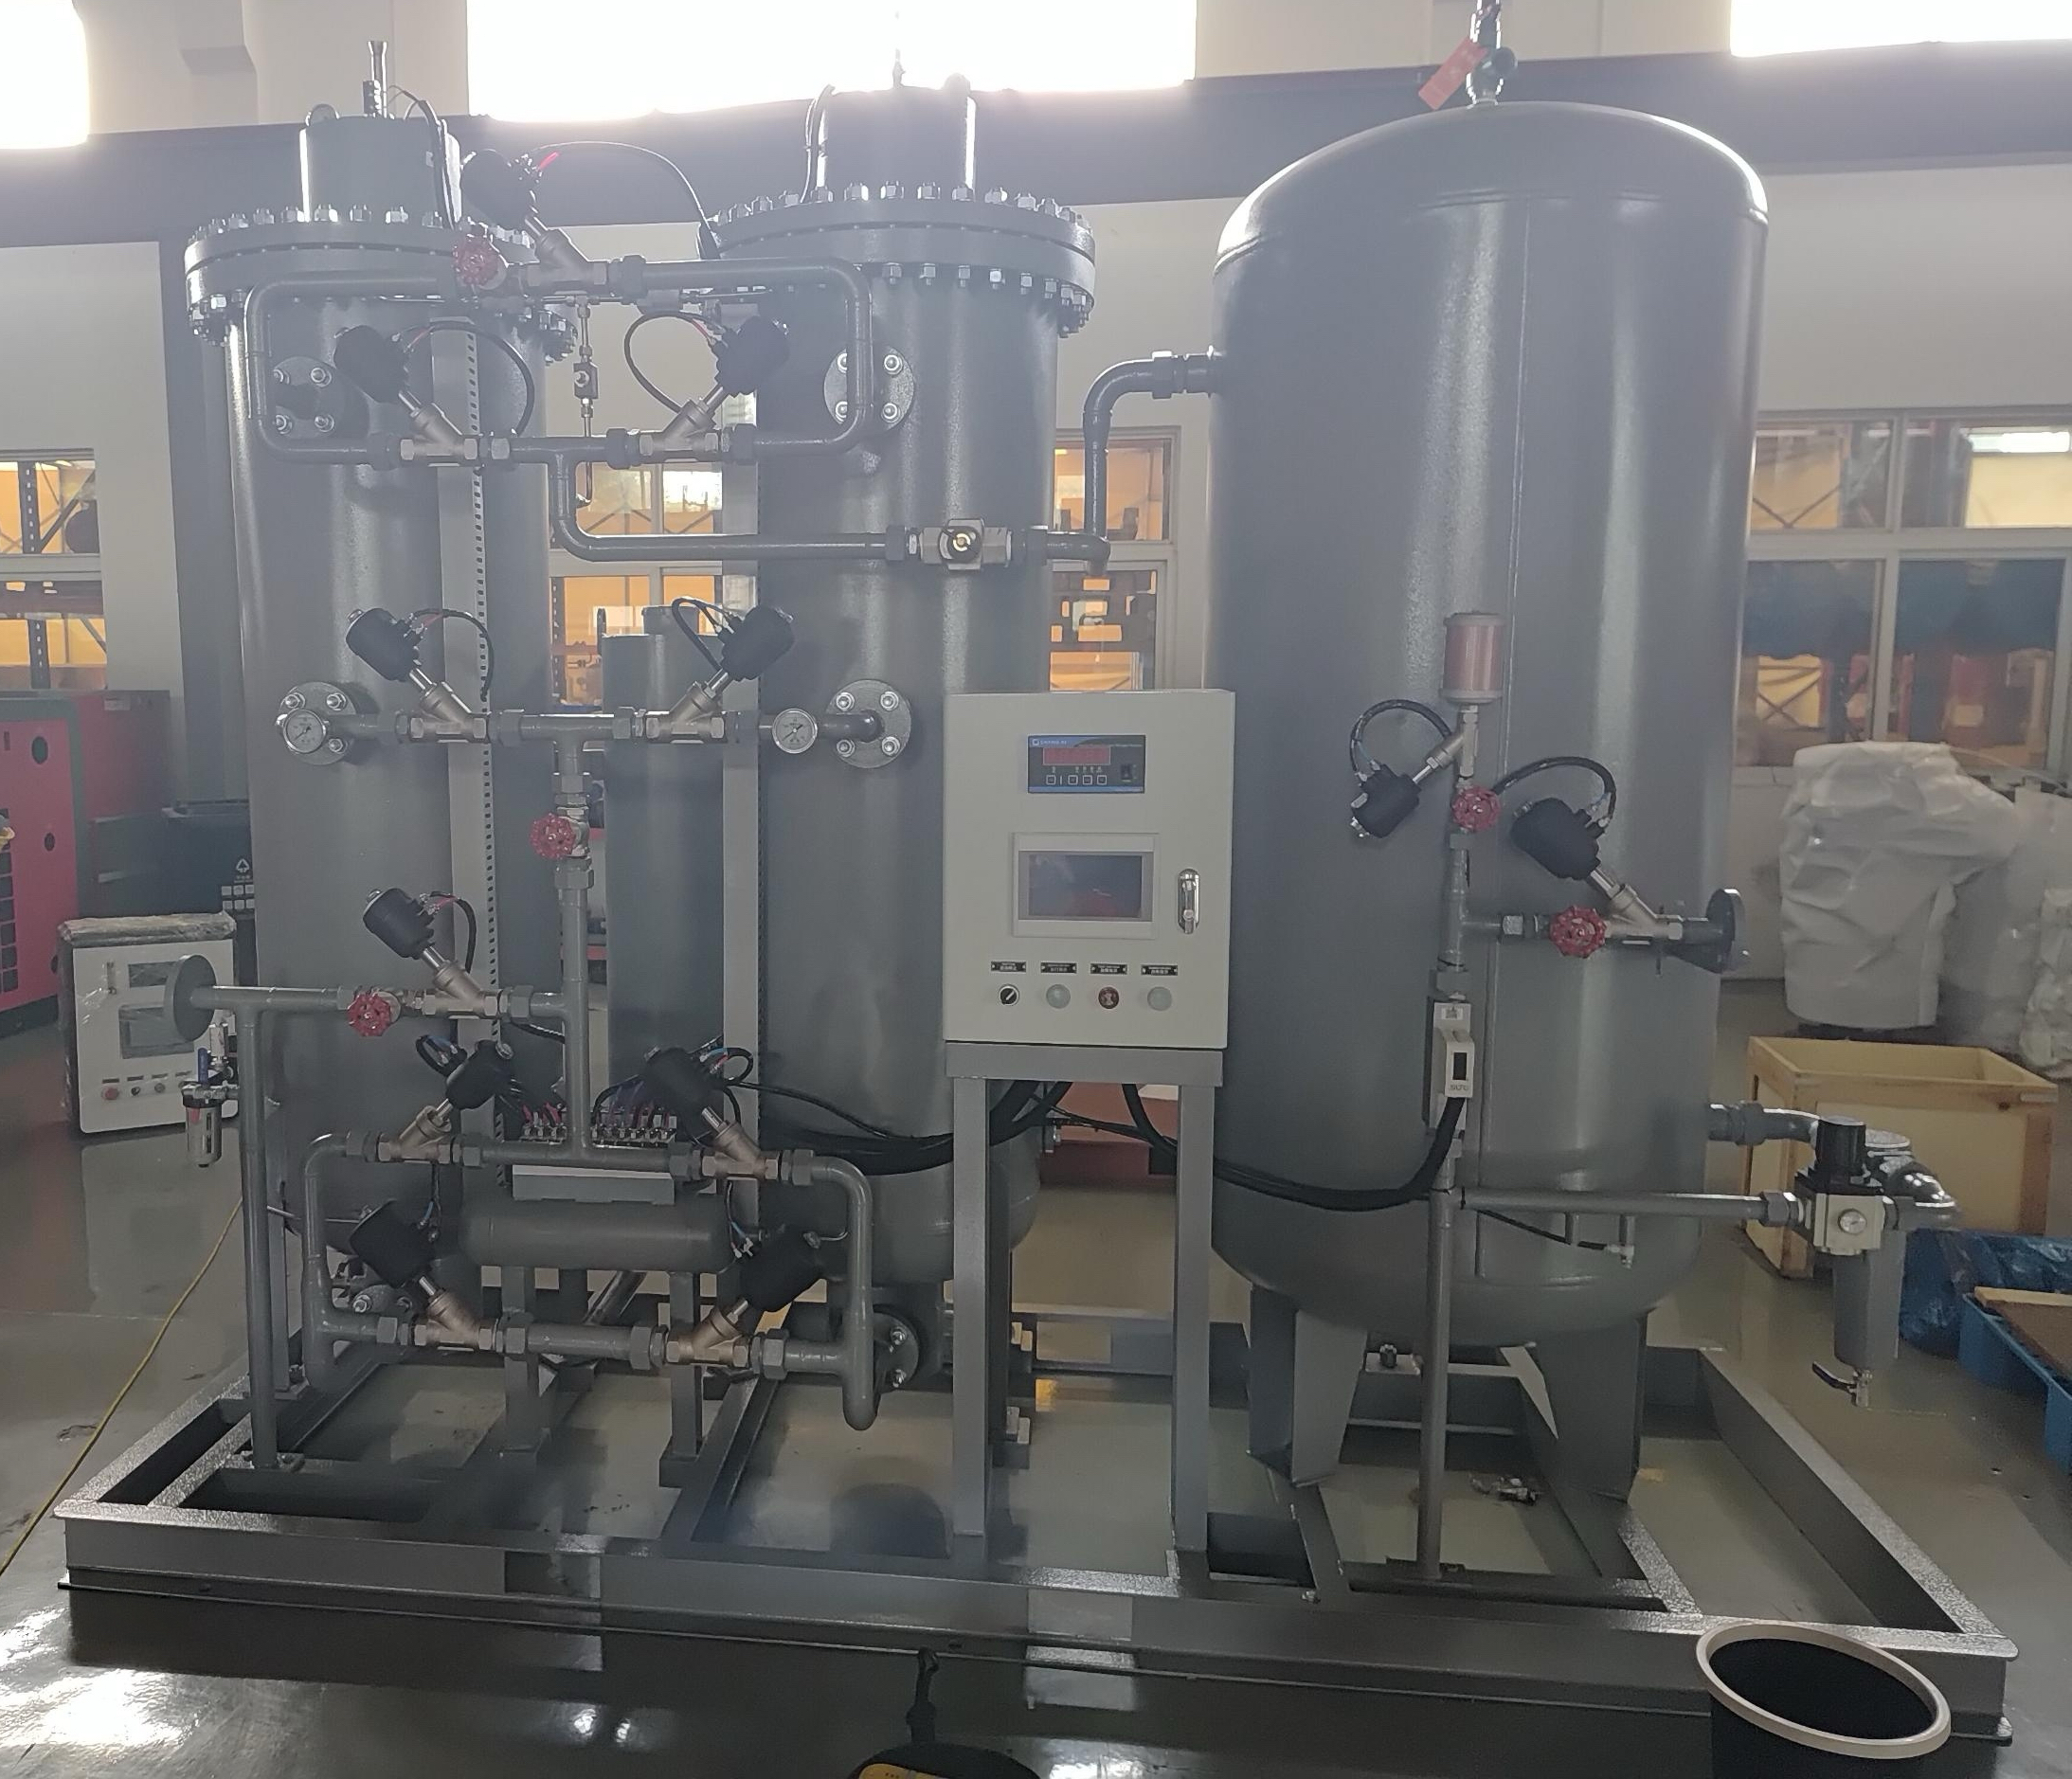
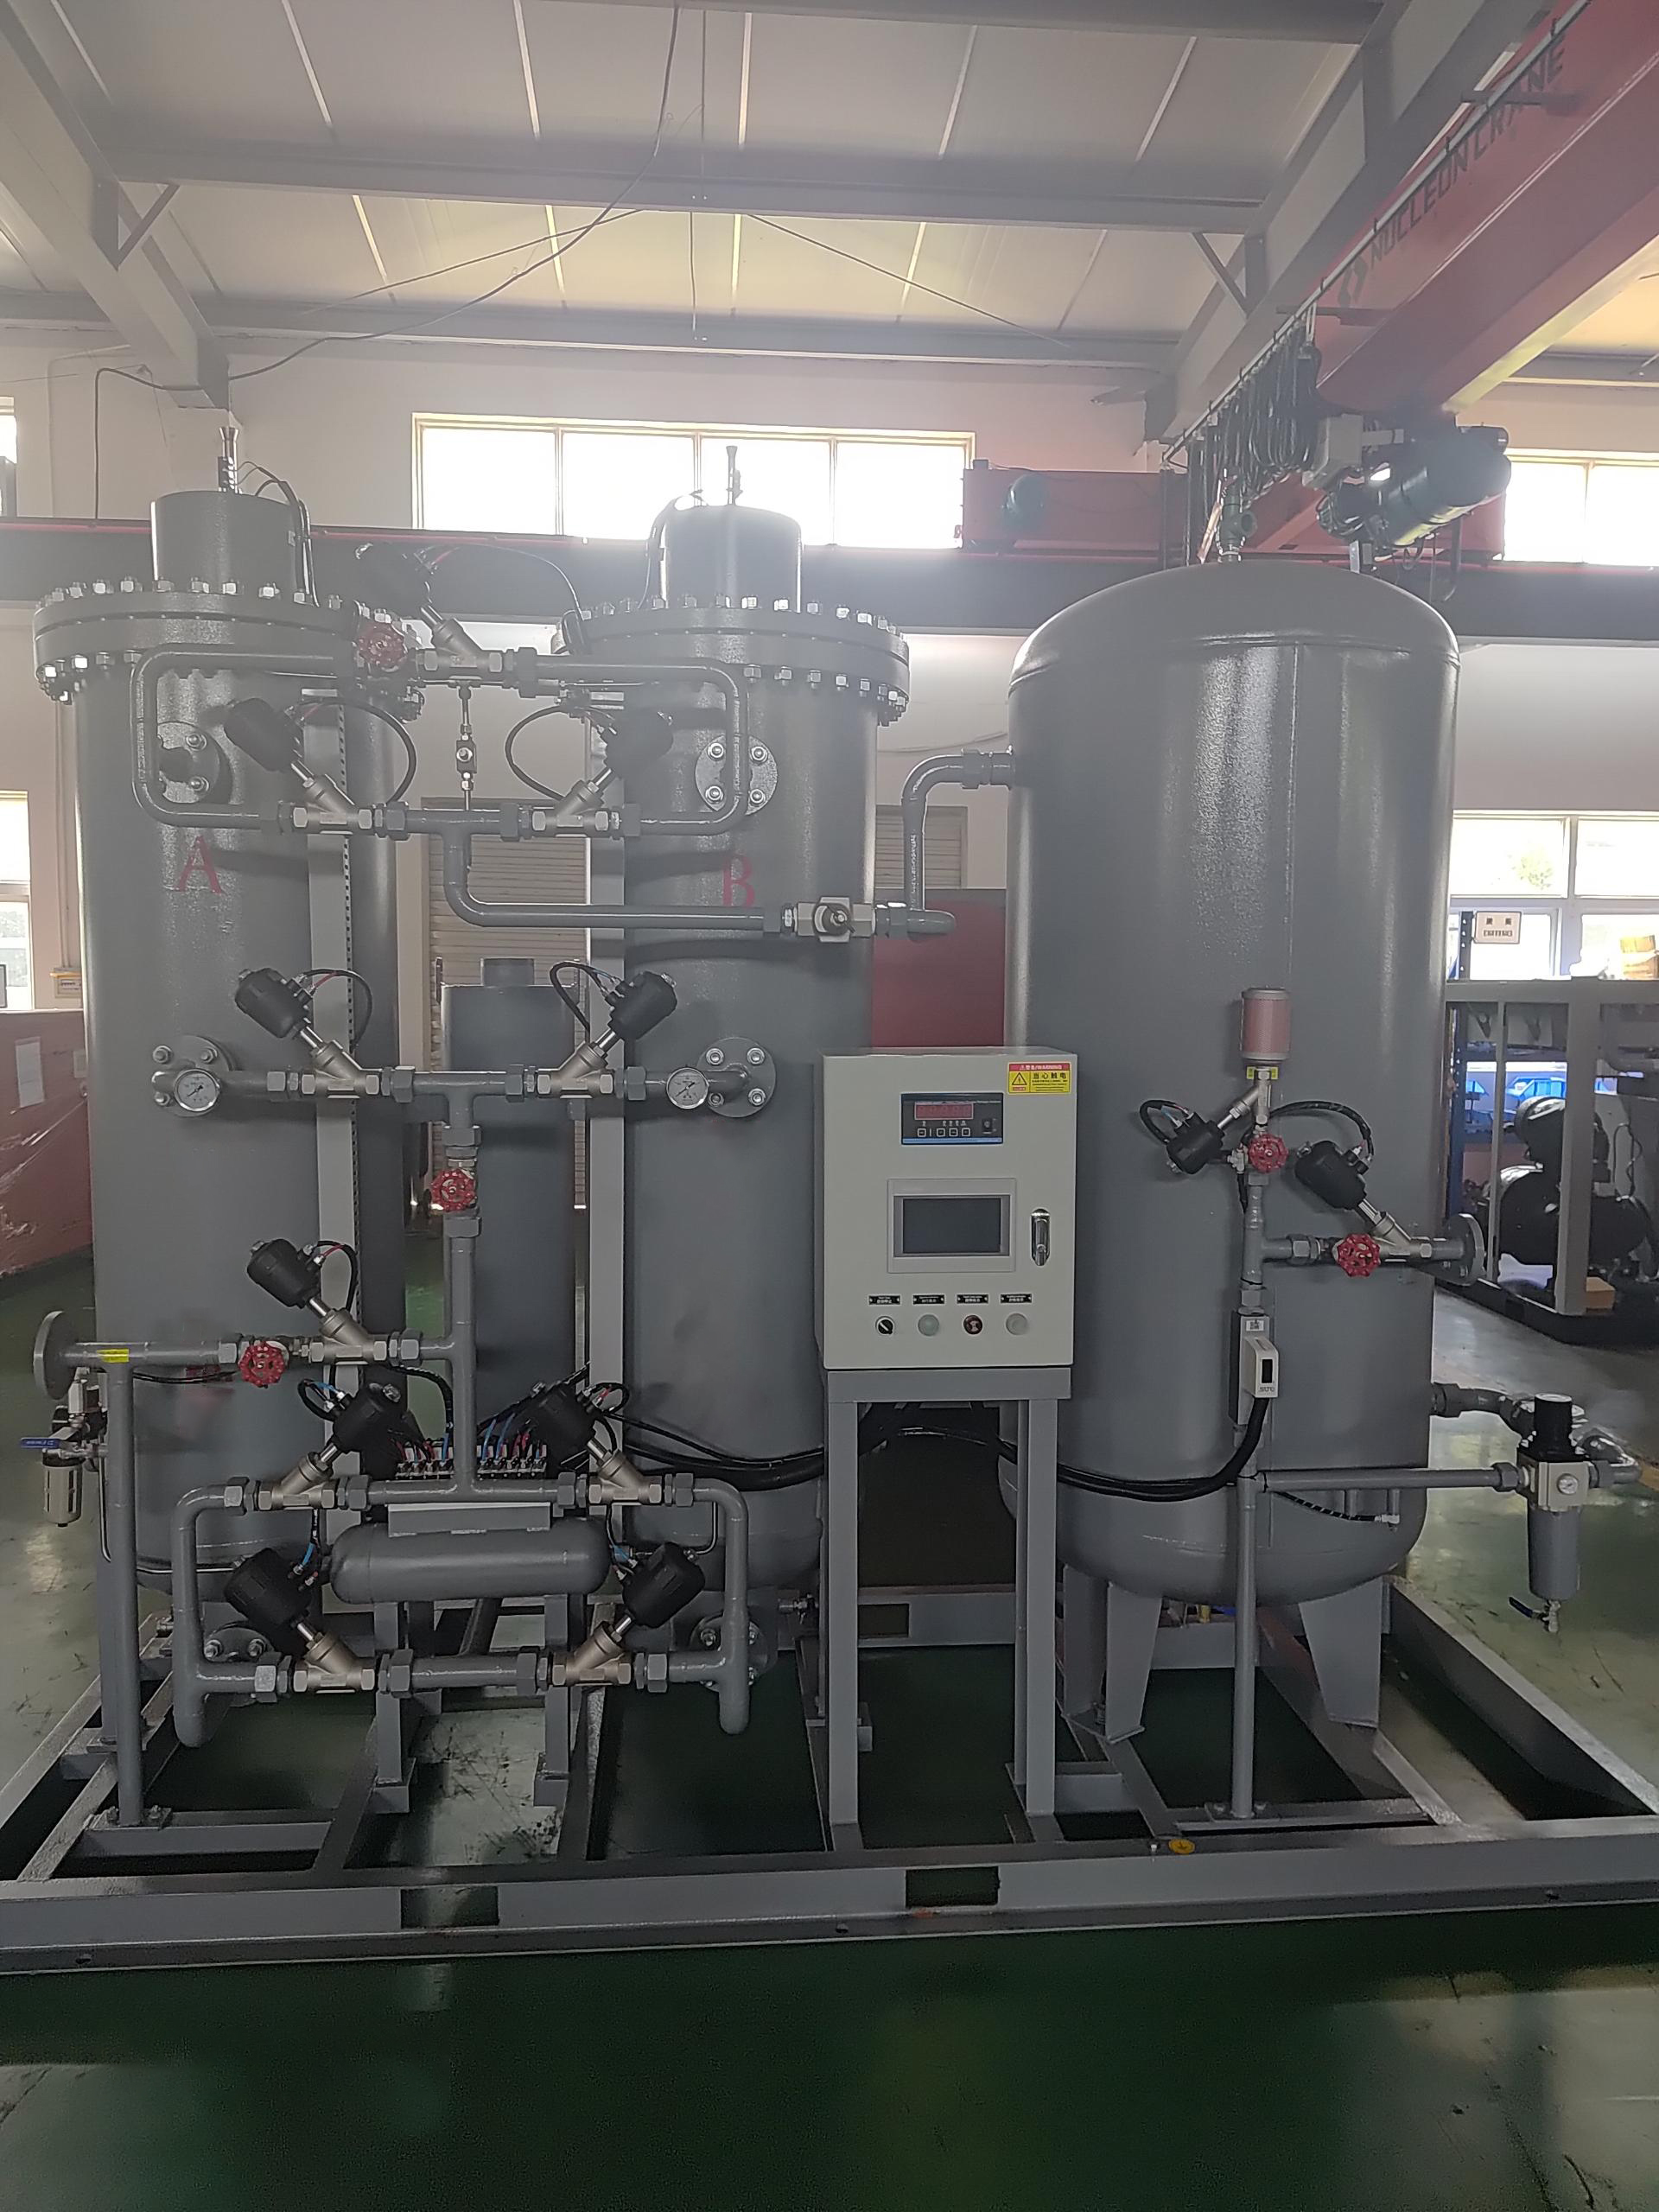
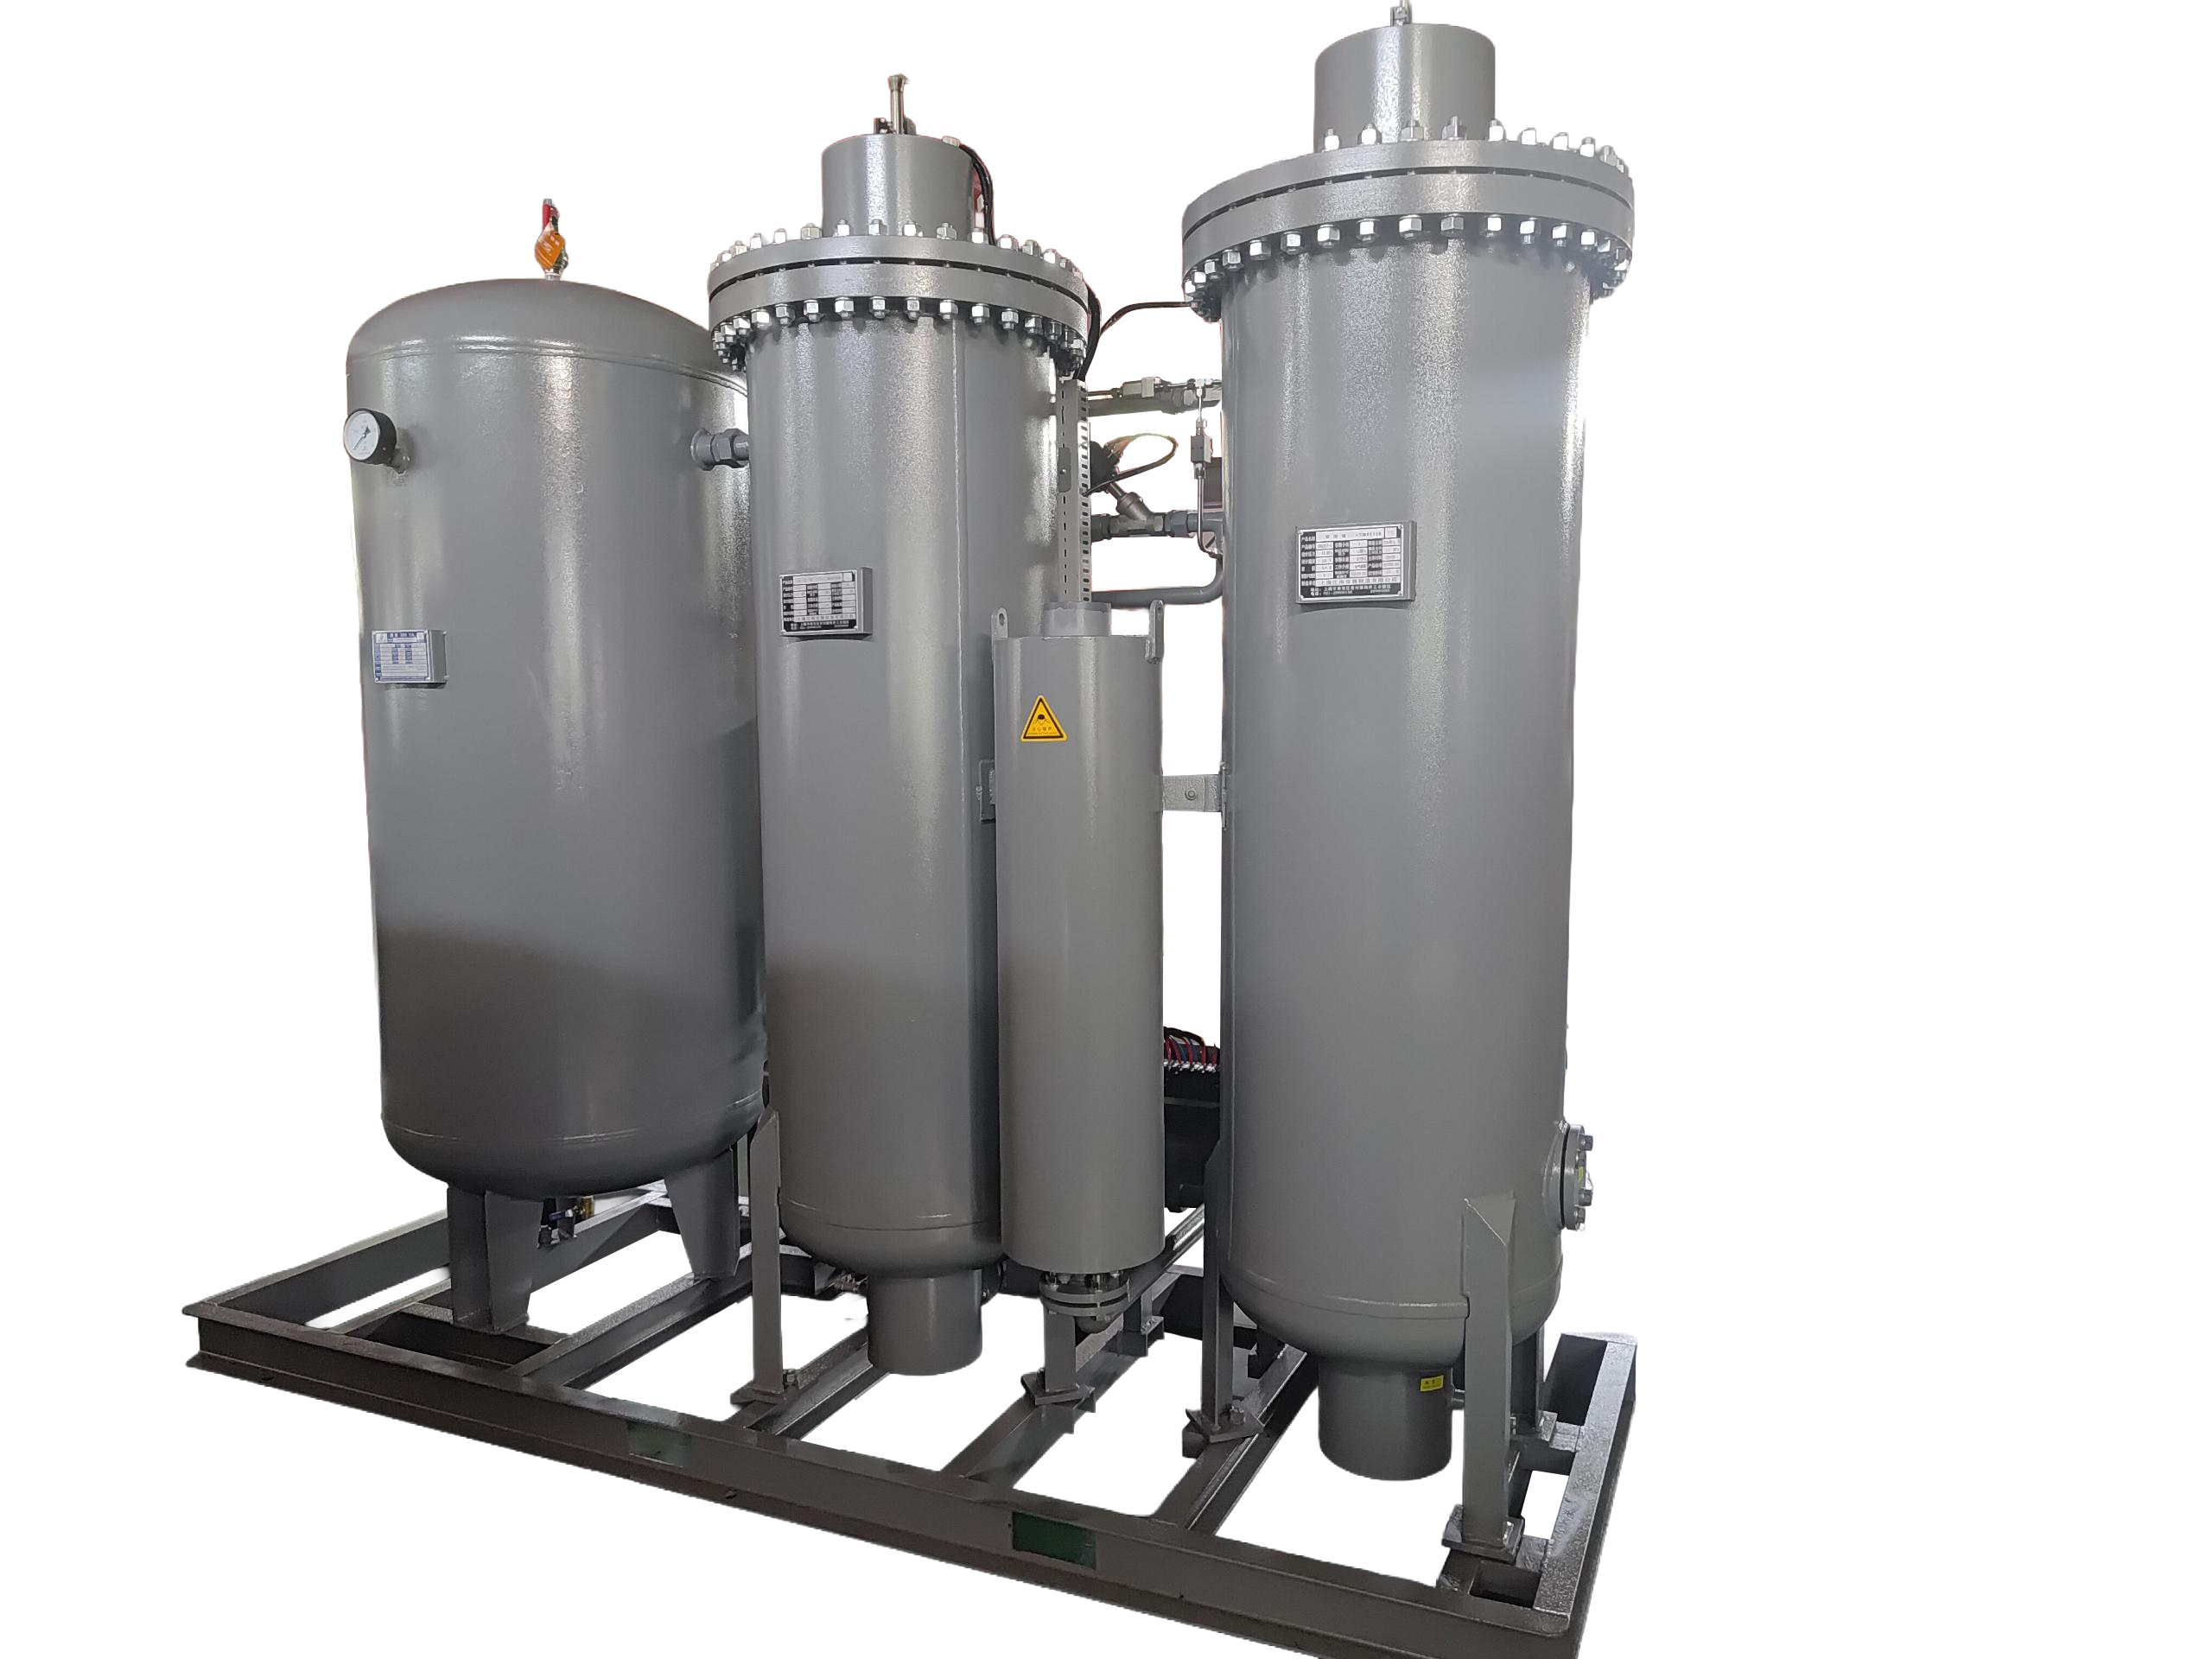
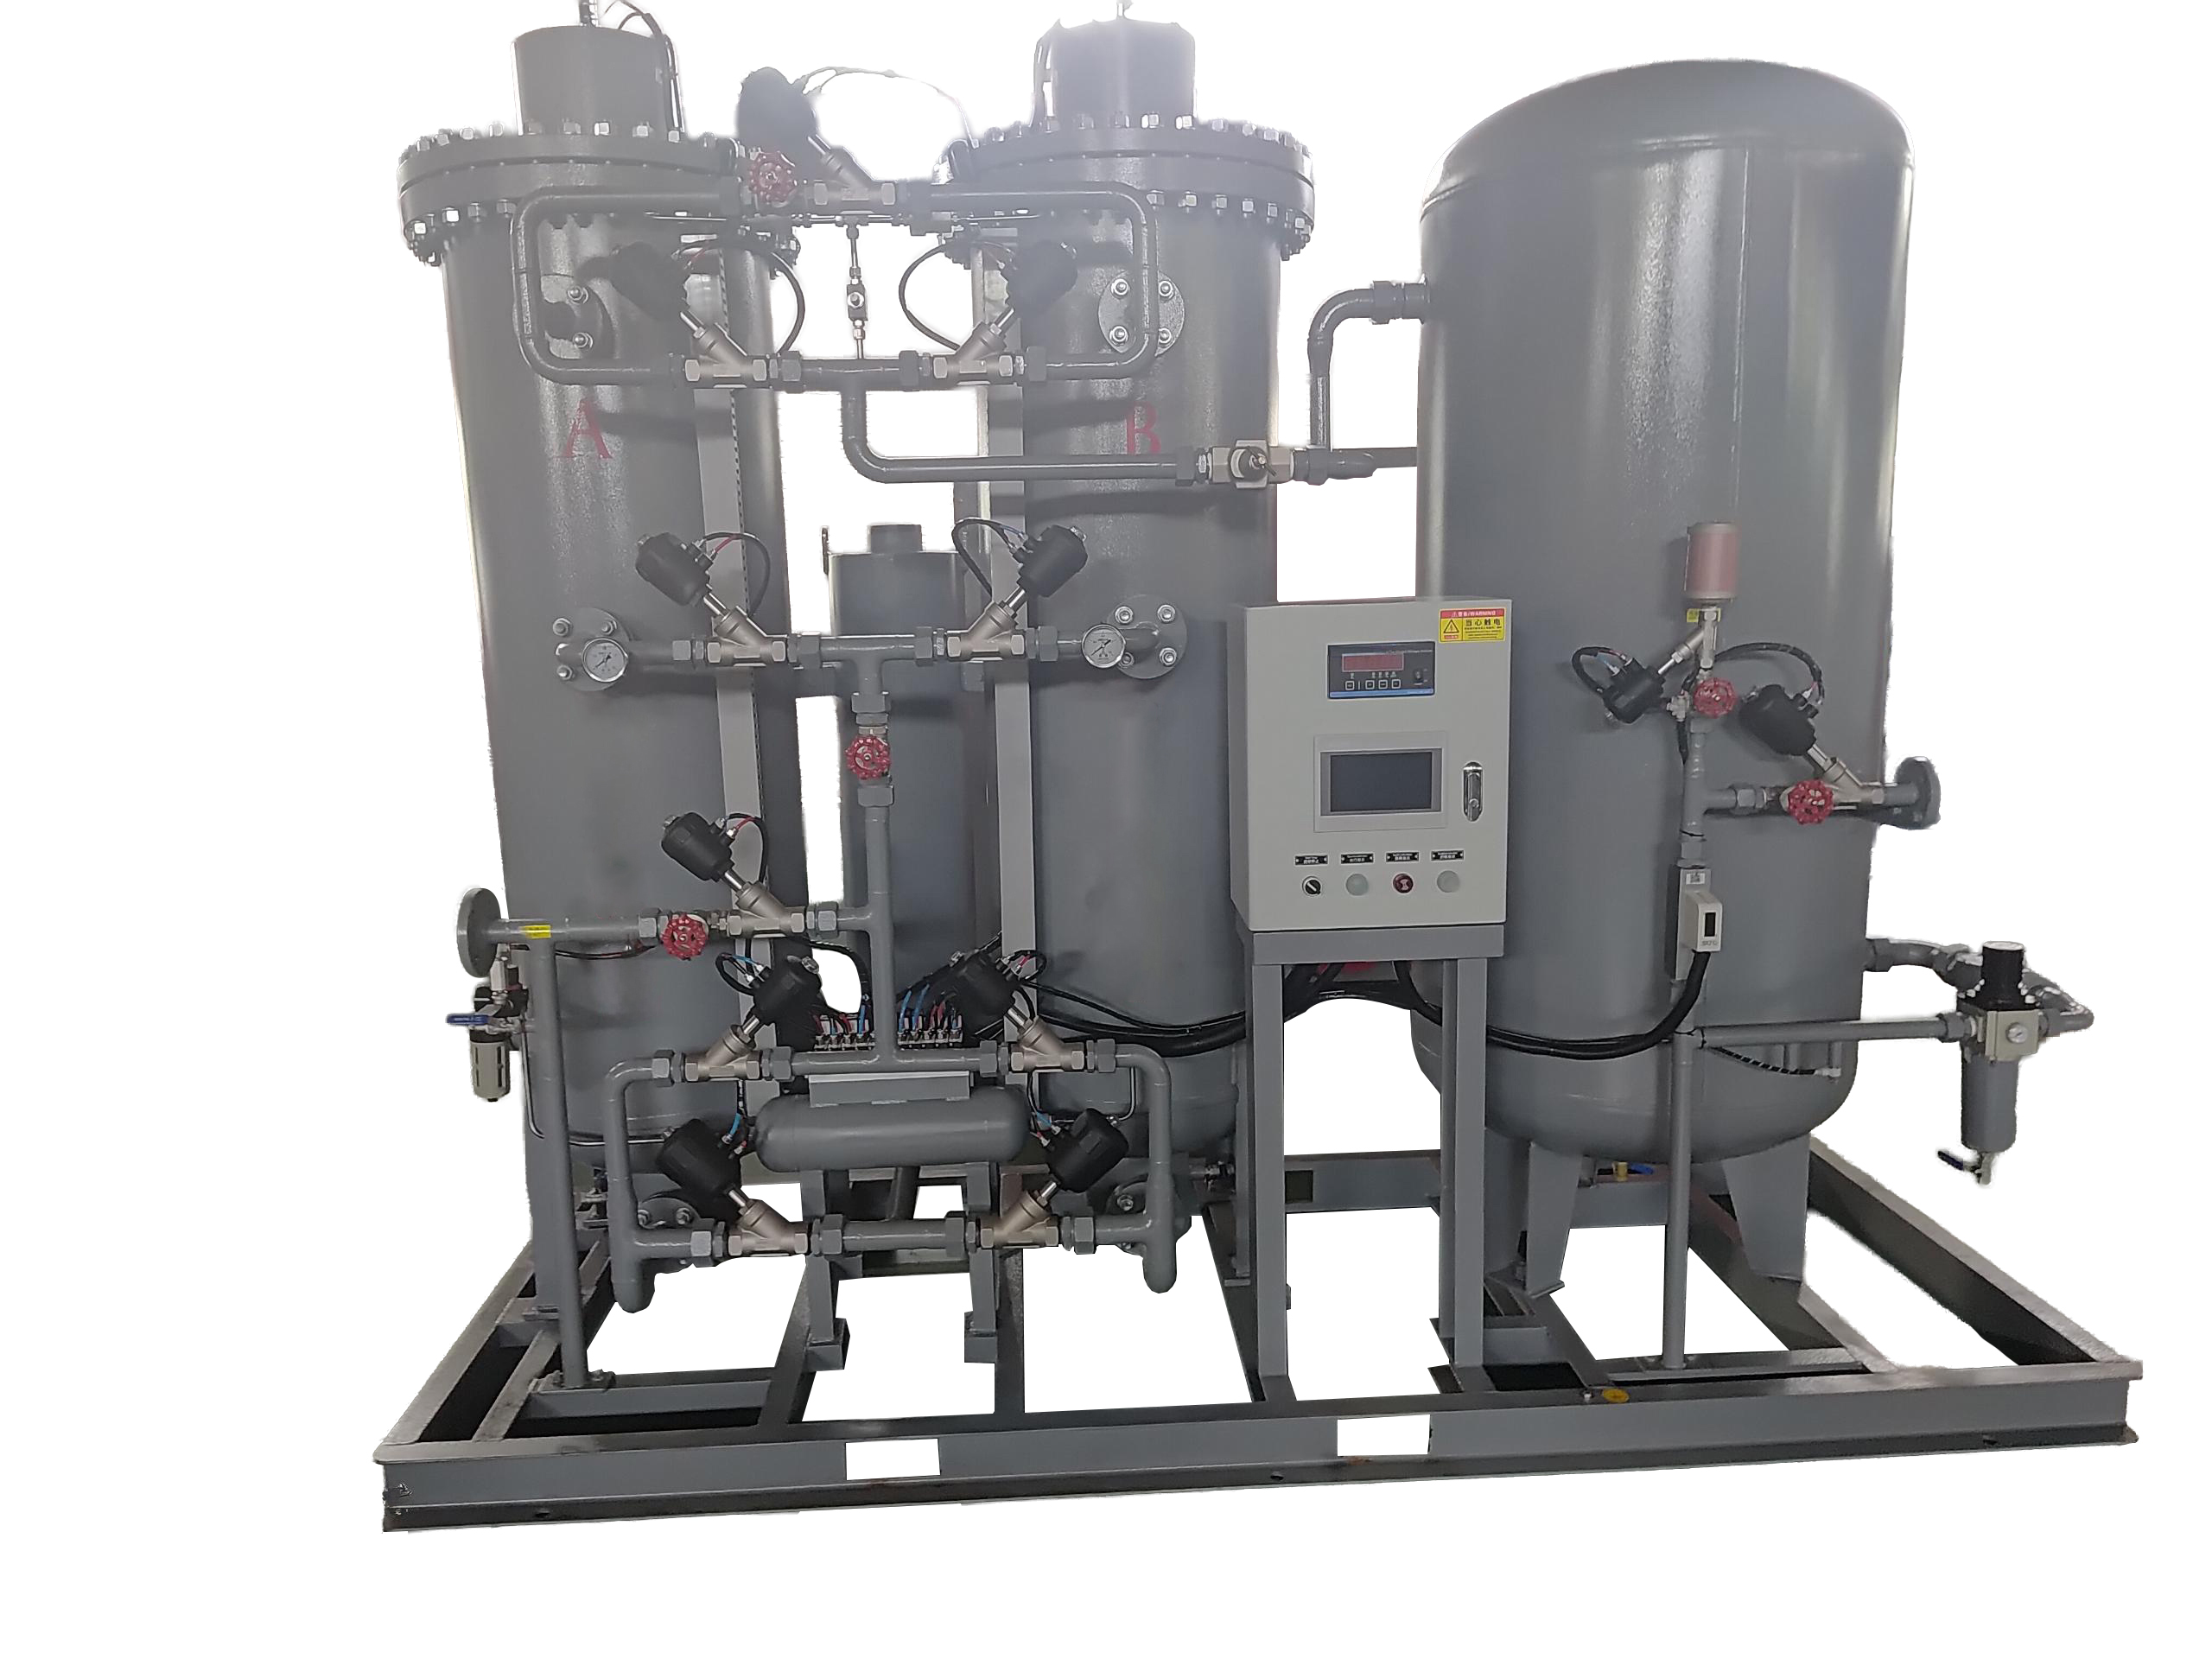
The system uses clean compressed air as the raw material and carbon molecular sieve as the adsorbent. Oxygen and nitrogen diffuse through the sieve pores at different rates, and this difference is what separates the two gases. A PLC controller alternates the twin adsorption towers between pressurized adsorption and atmospheric regeneration, so one tower always produces nitrogen while the other regenerates, giving continuous output at the required purity.
Black cylindrical particles roughly 1 to 2 mm in diameter, with micropores around 4 angstrom wide that adsorb oxygen far more readily than nitrogen. The smaller kinetic diameter of oxygen lets it diffuse faster into the sieve, while nitrogen passes through and is collected as the product gas.
Rather than the traditional top to top, bottom to bottom method, this design cross connects high purity nitrogen from one tower into the low pressure zone of the other, keeping a stable purity gradient and shortening the time to re-establish rated purity after each switch.
Valves open, close, and adjust automatically. No manual valve operation is required during normal running.
Live status, parameter setting, process switching, and fault display in one color touch screen.
Inlet pressure and carbon dust are monitored continuously, with automatic alarm and stop outside safe limits.
Out of spec gas triggers an automatic alarm, switches off supply, and vents until purity recovers.
Purity, flow, pressure, and optional dew point displayed in real time.
RS485 Modbus RTU for remote monitoring, with tiered operator permissions.
Stainless steel sleeve type valves operate from 0.3 MPa, switch in 0.3 to 0.5 seconds, and are rated for up to 3 million cycles. Angle seat valves add quick connect servicing.
A double ended design gives more even pressure distribution, with a stroke indicator and adjustable limit switches that trigger alarm or automatic stop.
Flow distribution is engineered to reduce dead zones and airflow disturbance at the sieve bed, cutting particle pulverization and extending sieve life.
Automatic alarm and shutoff below set purity, with off spec gas vented through a silenced outlet until back in range.
Suited to tire inflation, blanketing, and general purging where purity requirements are relatively loose.
A common choice for food packaging and laser cutting, where a moderate step up in purity supports process quality.
Used for electronics, lithium battery manufacturing, pharmaceutical processing, and precision heat treatment.
Higher purity places greater demand on the upstream compressor and air pretreatment, so system sizing matters more at this tier.
| Parameter | Range |
|---|---|
| Nitrogen purity | 97 percent to 99.9995 percent |
| Nitrogen flow rate | 1 to 5000 Nm3 per hour, sized to the model |
| Inlet pressure | 0.7 to 0.8 MPa |
| Inlet air temperature | Less than or equal to 30C |
| Nitrogen dew point | -40C to -60C, tighter values available on request |
| Rated power | From 0.2 kW depending on model |
| Power supply | 220V or 380V, 1 or 3 phase, 50 or 60 Hz |
| Control | PLC with HMI touch screen, RS485 Modbus RTU output |
Production capacity, adsorption tower size, weight, and footprint scale with model and purity. Full model by model tables covering every purity grade are available on request or in the complete product brochure.
Raw material handling, pipeline purging, gas replacement, and blanketing.
Food packaging, food preservation, and pharmaceutical packaging and storage.
Semiconductor manufacturing, integrated circuits, displays, and battery production.
Metal protection gas, welding shielding, heat treatment, and purging.
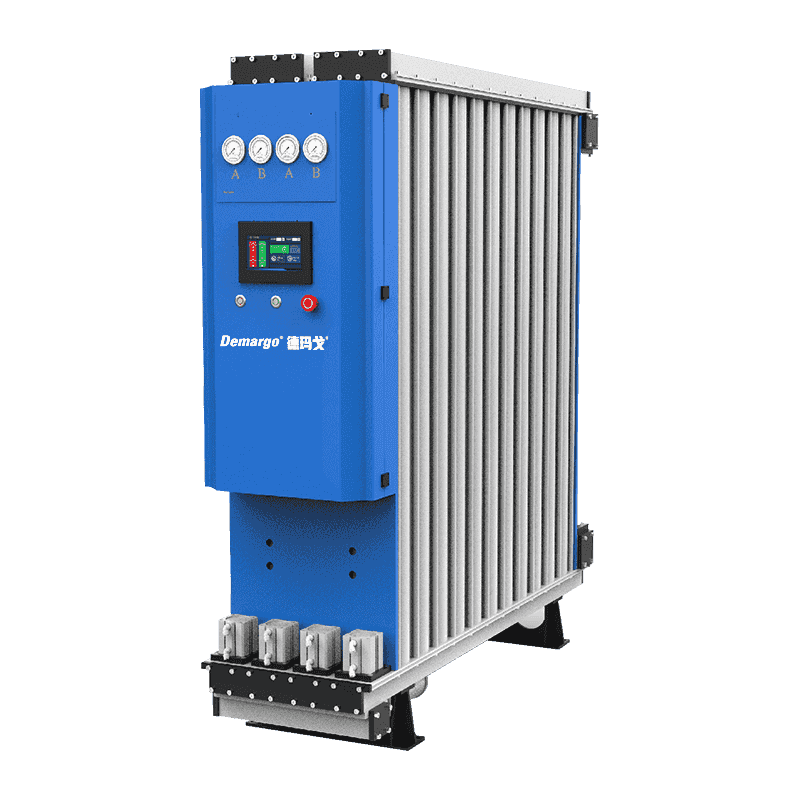
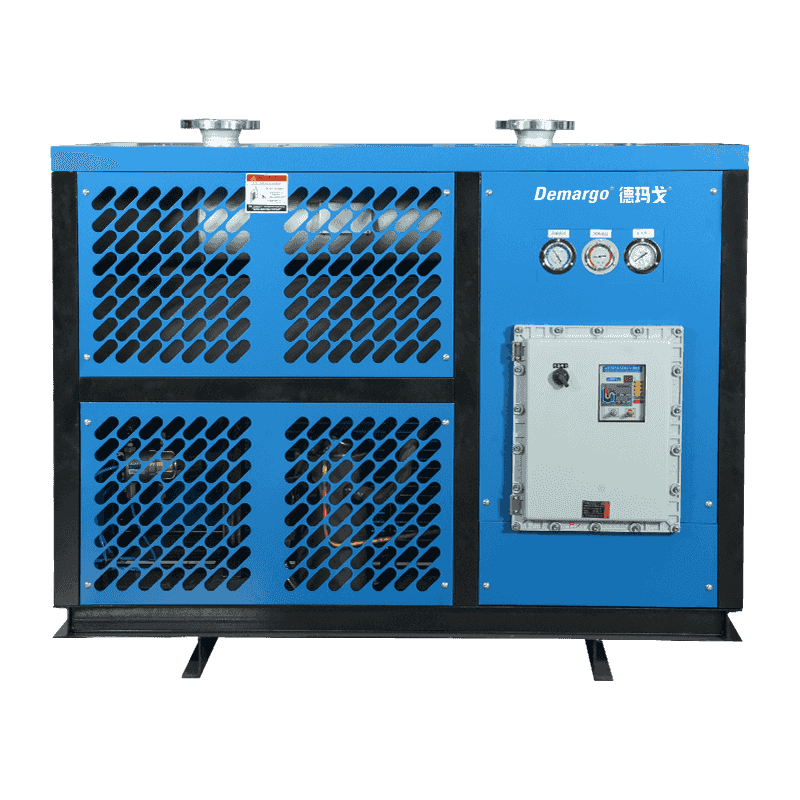
Air dryers, precision filters, and compressed air pretreatment are built in house, giving full control over the air quality feeding the nitrogen generator. Available as complete skid packages, OEM and ODM builds, or factory direct supply.
Unstable cylinder or liquid nitrogen deliveries, a true cost per unit of gas that is hard to pin down, and frequent cylinder changeovers. An on site generator converts that recurring supply cost into a fixed equipment and power cost, sized to actual demand.
Standard configurations cover 97 to 99.9995 percent nitrogen, depending on tower design and incoming air quality.
Selection is based on required purity, flow rate, outlet pressure, and dew point, matched against your existing compressed air supply.
The system monitors inlet pressure and carbon dust continuously and alarms or stops automatically outside safe limits.
Yes, the skid design connects to an existing or new compressor, dryer, filtration train, and storage tank, with Modbus RTU output for plant monitoring.
Yes, alongside standard skid packages, with air-cooled, water-cooled, high-temperature, variable frequency, and explosion-proof configurations.
Online monitoring triggers an automatic alarm and shutoff if purity drifts out of spec, with off spec gas vented until the system recovers.
Construction Cases
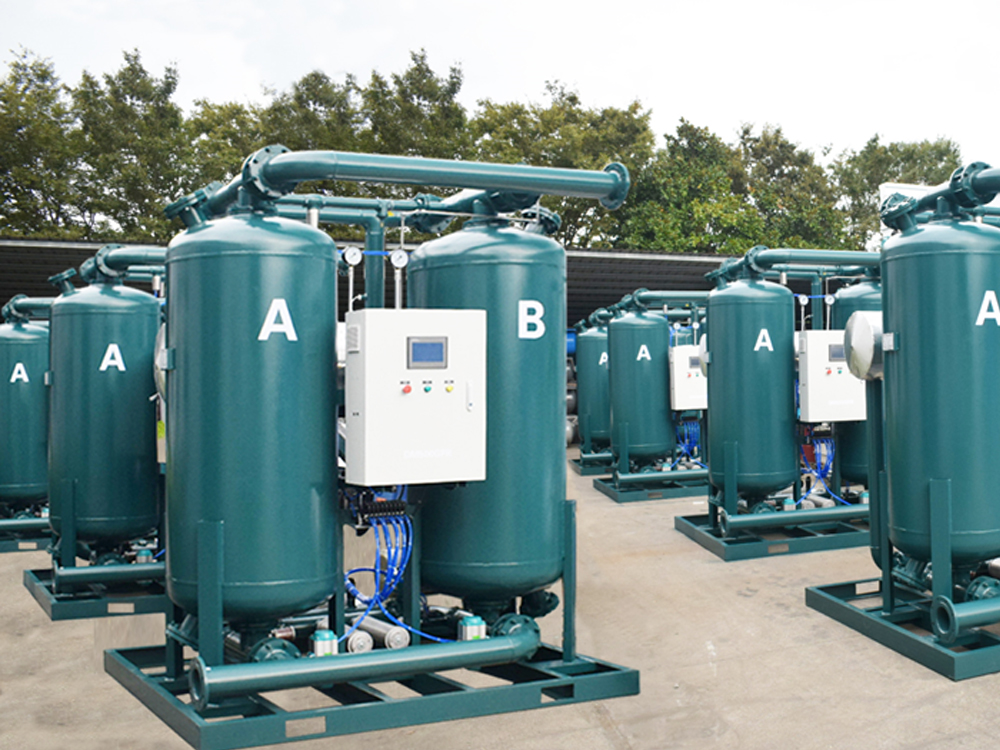
Dalian Dahua Group Co., Ltd.
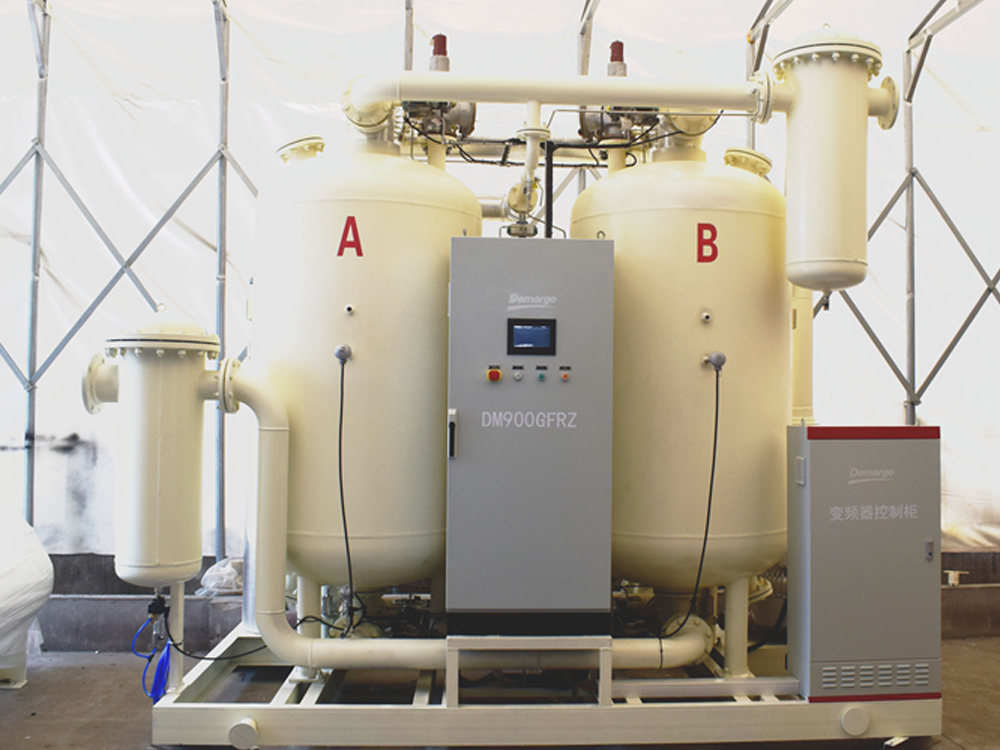
A large-scale electronic new material company in Jiangsu (Fortune 500)
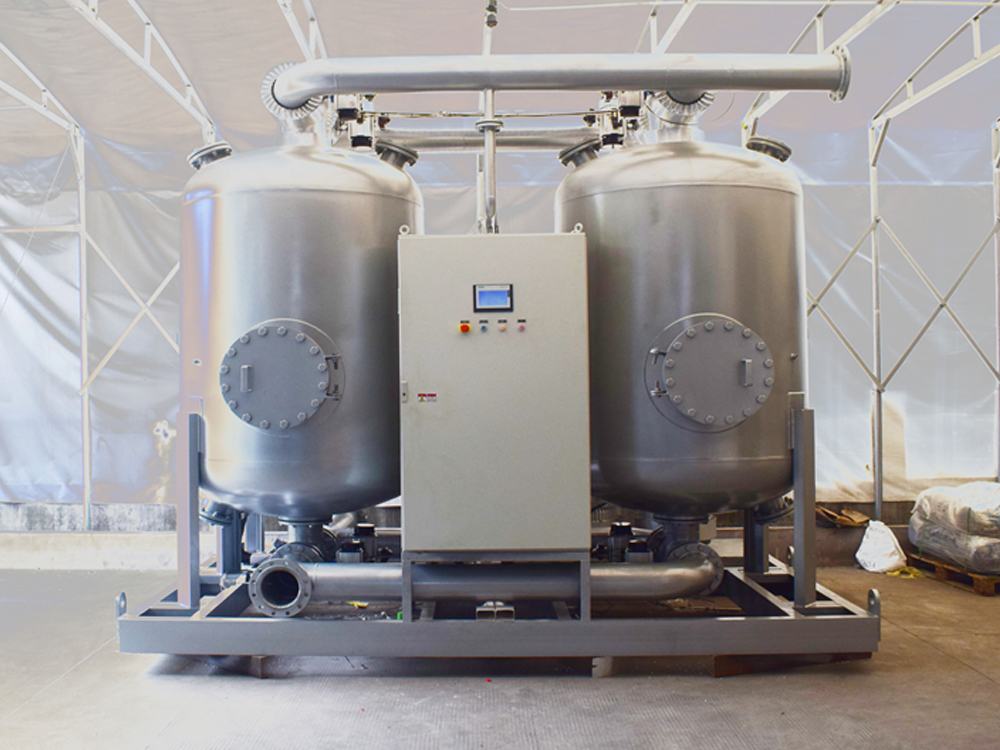
Shenyang Engine Research Institute
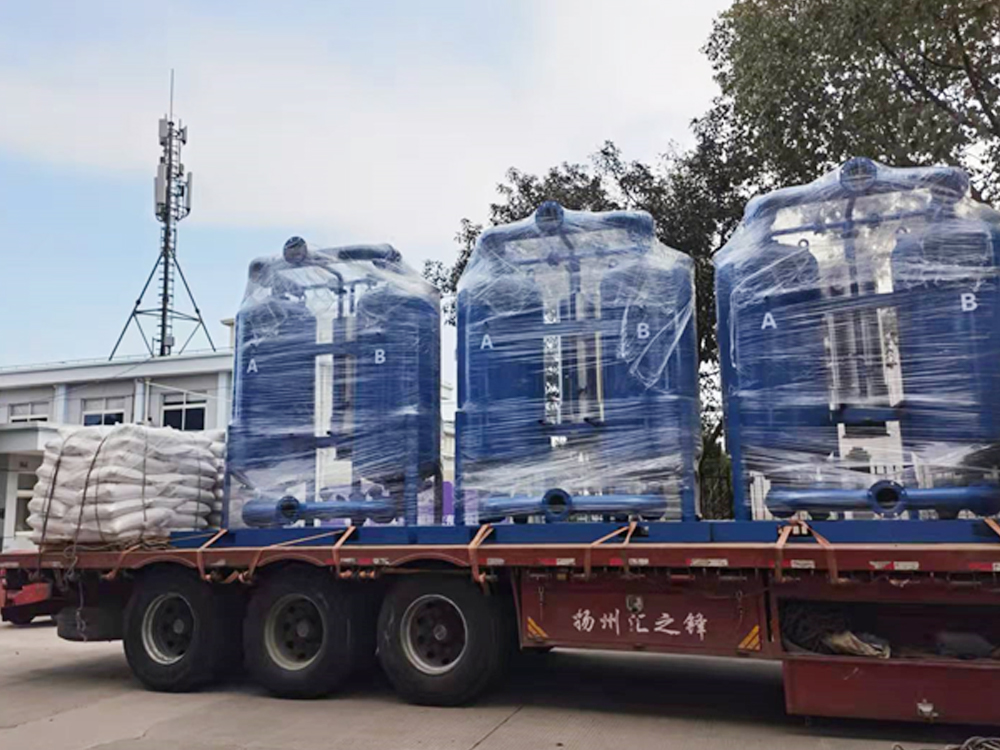
A large optoelectronics factory in Jiangsu
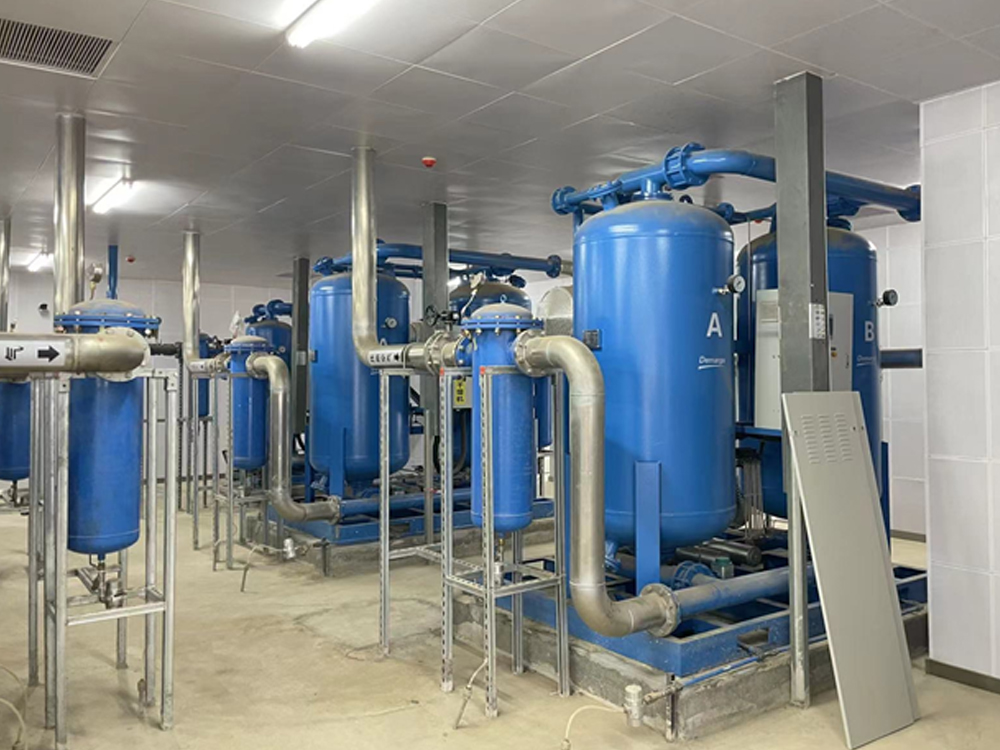
Hainan Haikou Airport
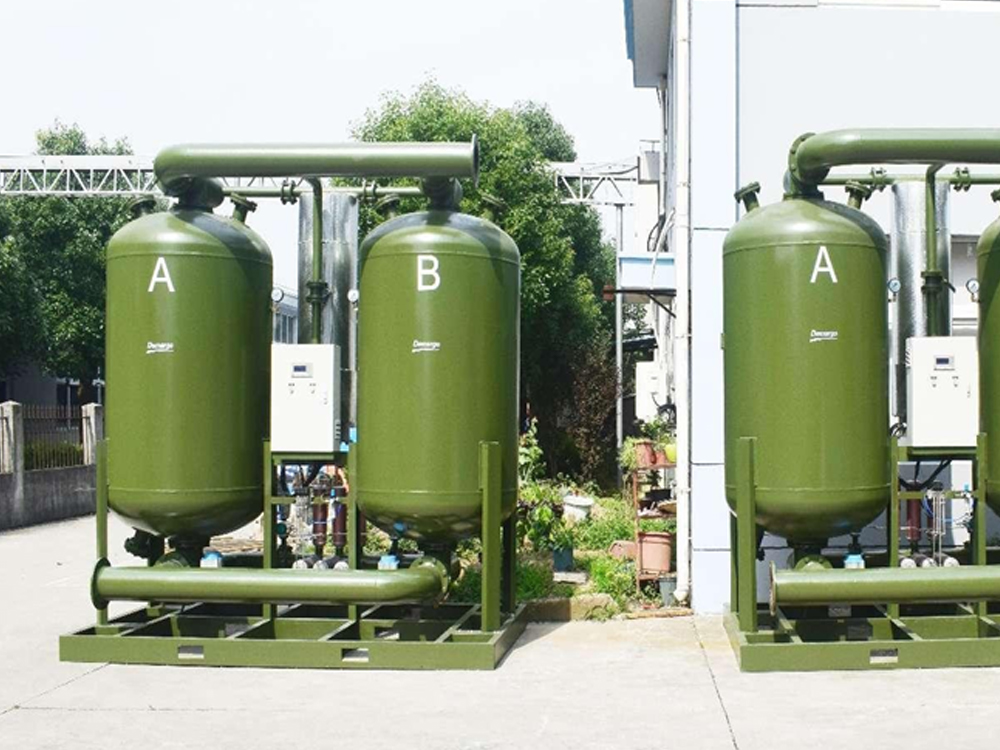
Equipment of a military factory in Shanghai
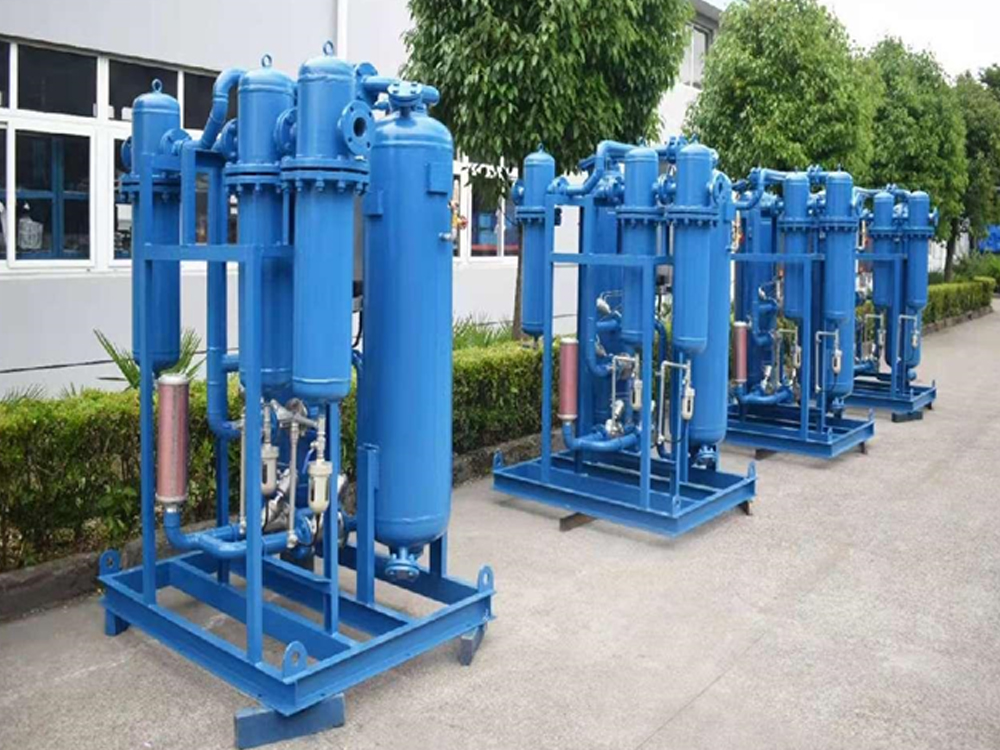
PetroChina offshore drilling platform
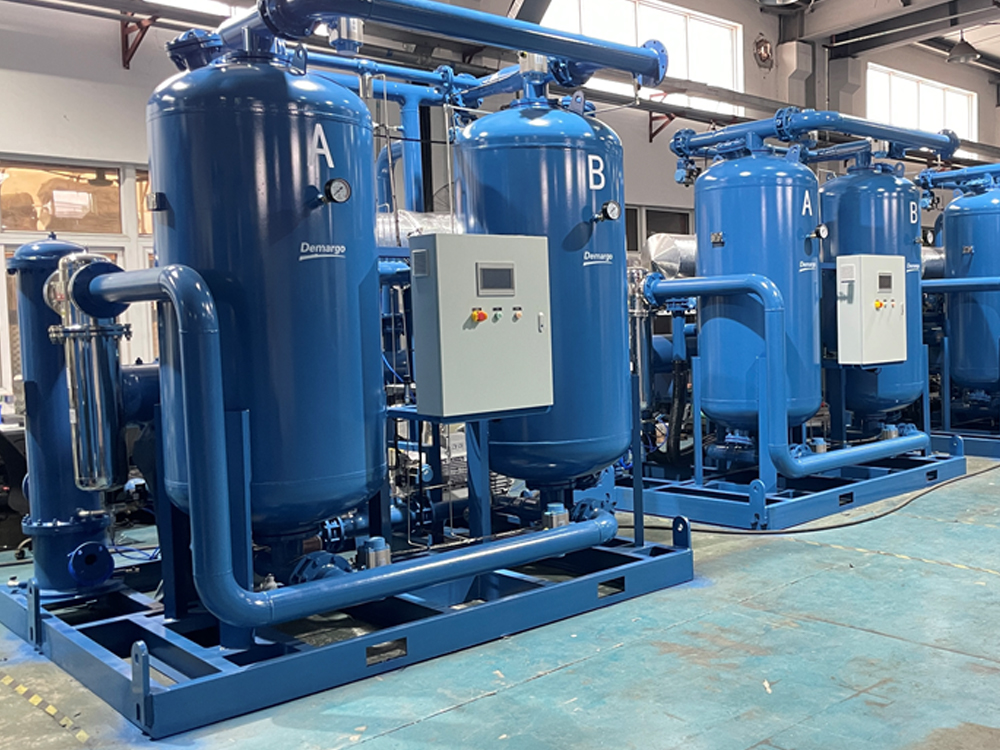
A chemical company in Shandong
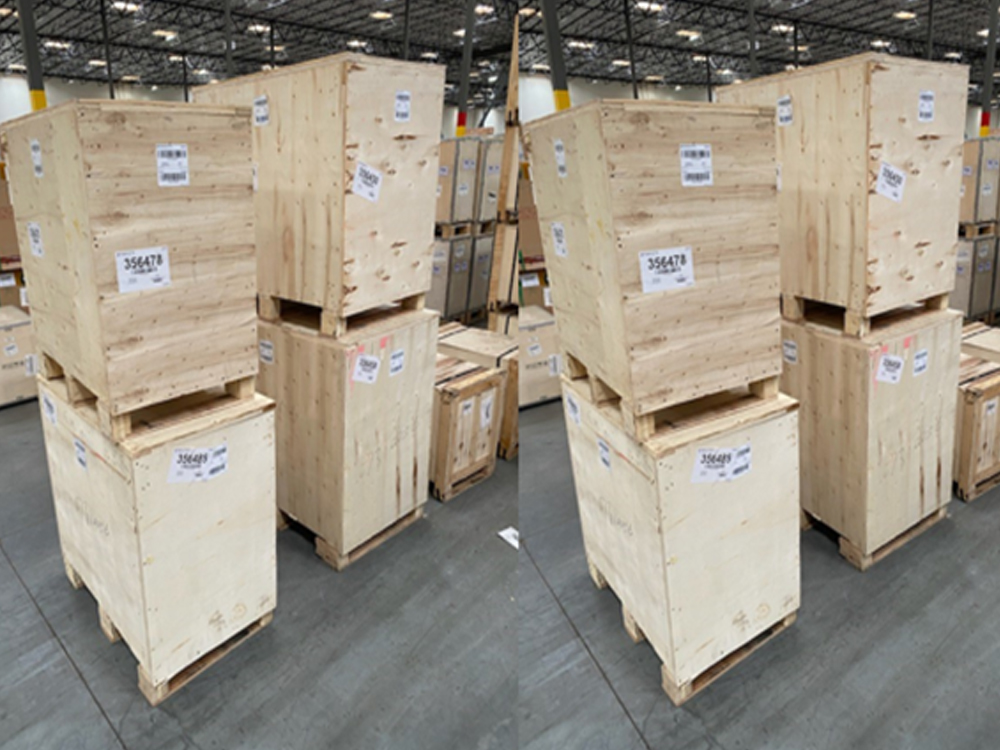
A company in California, USA
Contact Us for More Details
Don't hesitate to contact when you need us!
Related Products

At a petrochemical plant, a sticking control valve, a drifting analyzer, or a slow-acting emergency shutdown valve usually has one root cause: contaminated or ...
View MoreChemical process cooling equipment is not just about making process fluids cold. It is about controlling temperature precisely enough to protect reactors, stab...
View MoreA paper mill in Ontario was losing nearly $4,000 per month because condensation in its instrument air line kept fouling sensor valves across a single paper mac...
View MoreWhen you start comparing options for a new compressed air system, the first fork in the road is usually the same: should the compressor itself use oil for lubr...
View More
ADD: No. 9, Lane 38, Caoli Road, Fengjing Town, Jinshan District, Shanghai, China
Tel: 0086-17321147609
Email: [email protected]
Copyright © Demargo (Shanghai) Energy Saving Technology Co., Ltd. Rights Reserved. Wholesale Industrial High Purity PSA Nitrogen Generator Suppliers